Petroleum Fuel Storage Tanks At Terminals: An Engineering Company Guide
A fuel terminal is a hydraulic machine: tanker in, storage, tanker out, with product quality preserved at every step. The tanks are the most visible component and the easiest to get wrong — because the engineering that matters happens between them. Layout determines segregation and fire behavior; bunding contains the credible spill; transfer and vent systems determine whether the terminal runs at design throughput or limps at half of it.
This article covers the engineering decisions that define terminal-scale fuel storage: tank farm layout and separation, product segregation strategy, containment design, transfer and safety systems, and the project management discipline that keeps a depot build on schedule. It is written for owners, EPCs and operations teams evaluating tank supply for a terminal or depot.
Terminal-Scale Tank Farm Layout Principles
Terminal layout begins with flow: receipt, storage, blending where applicable, and dispatch. Tanks are grouped by product family and by fire zone, with radiant-heat-driven spacing between groups. Reception and dispatch areas sit at the terminal perimeter with dedicated truck lanes, so that tanker circulation never crosses loading points. For terminals above roughly 50,000 m3, hydraulic modeling of the transfer network is standard practice — pipe sizing, pump curves and valve losses are solved together, not tank by tank.
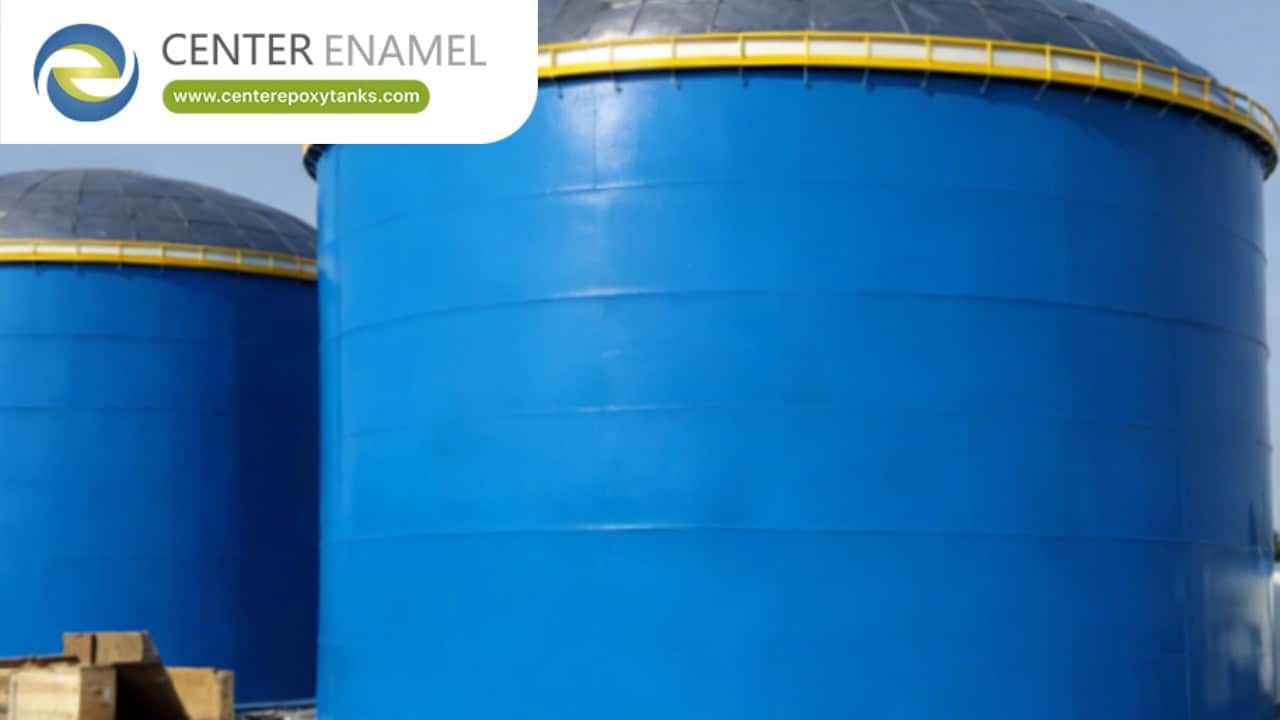
Bolt-on capacity changes the layout math. Bolted tank batteries can be extended in phases without welding into live structures, which is why phased terminals frequently standardize on factory-coated panel systems.
Product Segregation Strategy
Every segregated product needs dedicated tankage, dedicated piping and dedicated pump capacity, or a documented changeover procedure with heel management. Jet fuel is the strictest case: even trace contamination from gasoline or diesel service can fail specification testing, so jet tanks are frequently dedicated for life with restricted fittings and sealed manways.
Where segregation is by tank, shared-wall bunds are permitted under most codes provided the wall is tested and the smaller-tank rule for bund sizing is respected. Where segregation is by time, the heel volume, flushing protocol and batch testing regime must be written into operating procedures — not improvised.
Product | Segregation Requirement | Shared Tankage | Key Constraint |
Gasoline | Dedicated tankage or validated changeover | Possible with changeover | Vapor recovery, emission control |
Diesel | Dedicated tankage or validated changeover | Possible with changeover | Cloud point and filterability |
Jet fuel | Dedicated tankage for life | Not acceptable | Specification testing, filter integrity |
Biodiesel blends | Dedicated tankage | Not acceptable | Oxidation stability, microbial control |
Bunding And Diking: The Containment Calculation
Bund capacity is the single most audited number in terminal design. The common basis is 110 percent of the largest tank in the bund, plus allowances for precipitation and firewater where applicable. Bund walls must be hydrostatically tested before commissioning, penetrations must be sealed and documented, and drainage — where permitted — must pass through a closed valve with an interlock or an operator procedure that prevents inadvertent opening.
For bolted tank farms, bund walls are frequently fabricated from the same panel technology as the tanks, which accelerates construction and gives a uniform coating system. Foundations must be engineered for the combined tank-plus-full-bund load case; this is where bolted and welded terminals diverge most in civil scope.
Transfer Systems And Hydraulic Design
Terminal transfer systems are sized for the maximum simultaneous movement: receipt while dispatching, or blending while receiving. Pipe velocities are kept in the 1-3 m/s band — high enough to avoid water and sediment accumulation, low enough to control static generation. All piping is bonded and grounded; in Zone 1 and Zone 2 areas, flange and joint bonding is inspected, not assumed.
Tank outlet design deserves specific attention. Suction nozzles sit above the sump dead stock with sufficient submergence to avoid vortexing; water draw sumps are separate and dedicated so that routine water removal never touches product piping.
Vapor Management At Terminals
Terminal-scale vapor control has two layers: tank breathing (P/V vents sized for maximum pump-out and fill rates) and fleet-wide vapor recovery during truck loading. Loading vapor balance or VRU (vapor recovery unit) systems are increasingly mandated for gasoline terminals; the tank vents must be sized to accept recovered vapor without pressure accumulation, which is a calculation frequently missed in retrofit projects.
Vent flame arrestors must be specified for the product group and inspected on schedule — a contaminated or corroded arrestor is worse than none, because it blocks the relief path it exists to protect.
Fire Protection And Area Classification
Terminals are classified into hazardous zones radiating from tank vents, manways and loading points; every electrical device inside those zones must carry the corresponding certification. Fire protection typically combines fixed foam systems on the largest tanks, cooling water for adjacent exposures, and hydrant or monitor coverage sized by the firewater demand calculation.
Bolted tank terminals integrate cleanly with these systems: roof-mounted foam chambers and cooling rings mount to standard panel details, and the panel bonding provisions satisfy grounding requirements without field improvisation.
Metering, Blending And Quality Assurance
Custody transfer metering is where terminal revenue is settled, so meter proving is a scheduled activity, not an occasional audit. Blending — increasingly common at distribution terminals — requires tankage compatible with both components plus in-line blending skids whose hydraulic transients are checked against tank vent capacity.
Quality assurance runs in parallel: tank samples on receipt and dispatch, laboratory testing against product specification, and batch traceability from tank to tanker. Jet fuel receives the strictest regime, including membrane and filter integrity testing.
Project Management For Depot Builds
Depot projects fail on interfaces, not on tanks. The civil works, the tank supply, the piping contractor and the electrical classification package all converge on the same footprint; the critical path usually runs through foundation acceptance and hydrotest scheduling. Locking the tank delivery sequence against foundation readiness — and holding a float for weather — is what separates an on-schedule commissioning from a six-month overrun.
Center Enamel manages terminal-scale projects with a single engineering point of contact from specification through commissioning documentation, including third-party inspection coordination and as-built coating records.
Bolted Vs Welded At Terminal Scale
Welded field-erected tanks remain the default for large crude and product terminals: no practical diameter ceiling, mature code framework, lowest cost per cubic meter at scale. Bolted tanks win where erection duration, labor availability or relocation potential dominate the decision — remote depots, military and contingency fuel farms, and phased terminals where capacity follows demand.
The honest engineering answer is often a hybrid: welded main storage for base load, bolted tanks for peak shaving, contingency and blending side-streams.
Attribute | Welded Field-Erected | Bolted Coated |
Diameter ceiling | Effectively unlimited | Bounded by panel catalog |
Erection duration | Months | Weeks |
Cost per m3 at scale | Lowest | Moderate |
Coating control | Field application | Plant application, per-panel records |
Phased capacity | Difficult to extend | Natural — add batteries |
Relocatability | No | Yes |
Commissioning And Handover Documentation
Terminal commissioning is a documentation exercise as much as a construction one: hydrotest records, coating inspection reports, vent and arrestor certifications, calibration certificates for every meter and gauge, area classification drawings, and the integrity baseline that the operating phase will measure against.
Insist on the coating records. They are the only way future repairs can be matched to the original system, and they are the first document an insurer or regulator will ask to see after an incident.
Why Center Enamel For Terminal Fuel Storage
Center Enamel combines terminal-scale fabrication capacity with API 650 compliance and depot project management, delivering bolted GFS and epoxy-coated tank systems alongside engineering support for welded terminal scopes. Our coating systems are applied in controlled plant conditions and documented per panel, which is why our tanks hold specification in fuel service across more than 100 export markets.
For terminal projects, we support owners from capacity studies and layout reviews through commissioning documentation — engineering continuity that survives the handover.
About Company
Shijiazhuang Zhengzhong Technology Co.,Ltd(Center Enamel) is a professional manufacturer dedicated to the design and fabrication of bolted storage tanks since 2008. Our products range includes Glass-Fused-to-Steel (GFS) tanks, fusion bonded epoxy tanks, stainless steel tanks, galvanized steel tanks and aluminum geodesic dome roofs. With professional enameling R&D team and nearly 200 enameling patents, Shijiazhuang Zhengzhong Technology Co.,Ltd has become the leader in bolted tanks industry of Asia. Our products are certified to ISO9001, NSF61, EN1090, ISO28765, WRAS ,FM, LFGB, BSCI, IS0 45001 and other international standards.
Shijiazhuang Zhengzhong Technology Co., Ltd is not only the first manufacturer in China which produces Glass-Fused-to-Steel tanks, but also the most experienced professional bolted tanks manufacturer in Asia.The engineering & design, product testing and quality system of Center Enamel Glass-Fused-to-Steel tanks is in strict accordance with AWWA D103-09, OSHA, ISO 28765, NSF/ANSI 61, NFPA and other international standards. Until 2023, Center Enamel bolted tanks have been exported to more than 100 countries including USA, Australia,Canada, Malaysia, Indonesia, Russia, UAE, Panama,Brazil and South Africa etc., the superior tank quality and prompt service gains us worldwide recognition.
As an outstanding containment and cover system provider with decades of industry experience, Shijiazhuang Zhengzhong Technology Co., Ltd sincerely expects to establish long-term cooperation with the local partners throughout the world and make continuous contribution to the development of the industry.
Suggested CTA
Center Enamel delivers welded carbon steel engineered for gasoline, diesel and jet fuel storage duty, with terminal-scale fabrication capacity, api 650 compliance, project management for depots. Contact our engineering team for selection and procurement guidance on your next petroleum fuel storage tanks project — including sizing, standards compliance and delivery scheduling.
Frequently Asked Questions
Q: How many tanks does a fuel terminal need?
A: At minimum one dedicated tank per segregated product, plus peak-shaving and contingency volume. Jet fuel almost always requires dedicated tankage; other products can share tankage through documented changeover procedures with heel management and batch testing.
Q: What bund capacity is required at a fuel terminal?
A: The common basis is 110 percent of the largest tank within the bund, with additional allowances where firewater or precipitation accumulation is credible. Bund walls must be hydrostatically tested before commissioning and all penetrations sealed and documented.
Q: Are bolted tanks compliant for gasoline and diesel storage?
A: Yes, where the panel coating is verified compatible with the product. Bolted GFS and epoxy-coated tanks are widely deployed for diesel, kerosene and gasoline-adjacent service; ethanol blends and sour streams require coating compatibility verification before specification.
Q: What is the difference between a depot and a terminal?
A: In common usage, a terminal is a larger receipt-storage-dispatch facility with pipeline or marine receipt, while a depot is a smaller road-receipt distribution facility. Engineering requirements are the same in kind; scale, metering scope and fire protection sizing differ.
Q: How is vapor handled during truck loading?
A: Through vapor balance systems returning displaced vapor to tankage, or through vapor recovery units that condense and recover it. Tank vents must be sized to accept the recovered vapor at maximum loading rate — a calculation frequently missed in retrofits.
Q: What documentation should a terminal handover include?
A: Hydrotest records, panel coating inspection reports, vent and flame arrestor certifications, meter calibration certificates, area classification drawings, bonding and grounding inspection records, and the integrity baseline for the operating phase.