Durable Oil Reserve Tanks - Designing for Decades of Standby and Sudden Duty
A reserve tank has the most demanding duty in storage: sit for years, often full, then perform on demand. That duty punishes anything that degrades with time - coatings that age while the tank is idle, water bottoms that corrode unseen, seals that take a set, and instrumentation that is never exercised. It also punishes maintenance models that assume a convenient outage, because a reserve tank's outage has to be someone else's schedule.
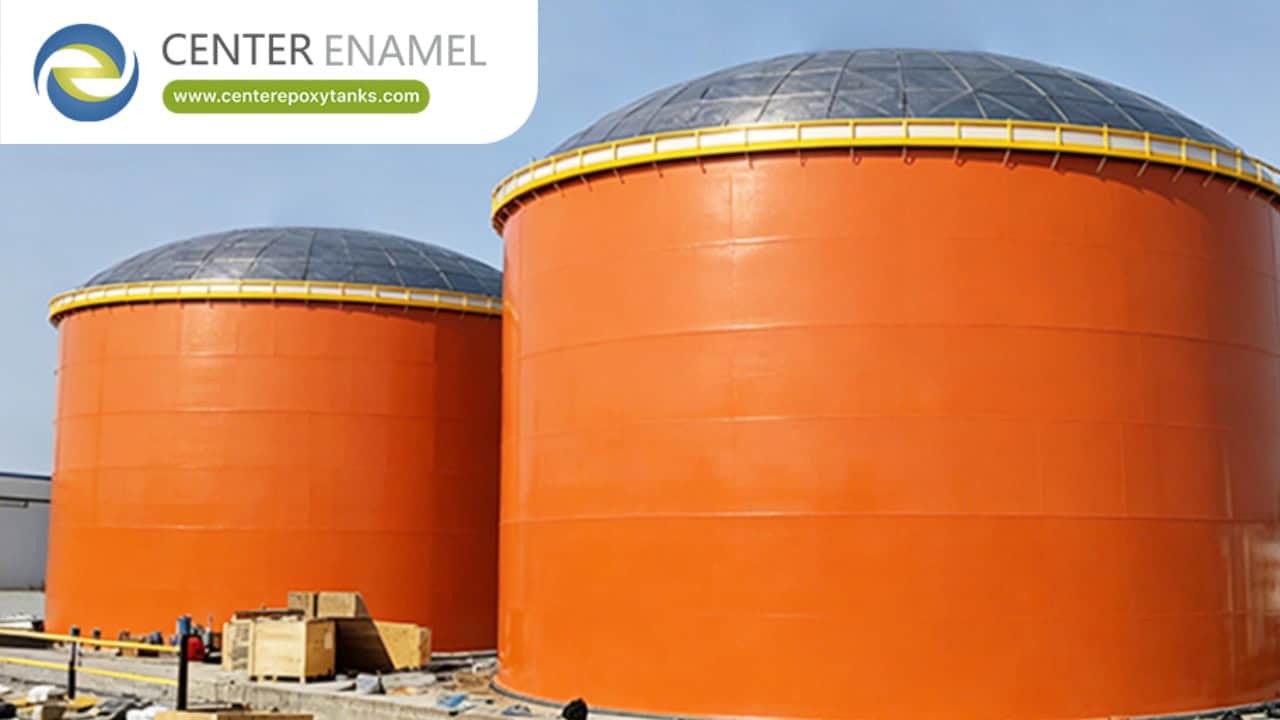
Engineered by Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel), durable oil reserve tanks are designed so that the things which degrade with time are either removed or made inspectable without emptying the tank.
1. What Makes a Reserve Tank Durable?
Adequate corrosion allowance, a coating and cathodic protection system that lasts, water management that prevents the dominant corrosion mechanism, and details that can be inspected or renewed without a full outage.
· Corrosion Allowance: Sized for the full design life, not for a typical commercial interval.
· Coating System: Selected and applied for very long service, over verified surface preparation.
· Cathodic Protection: Designed for the site and monitored, covering coating defects for the life of the tank.
· Water Management: Draw-off and exclusion prevent the corrosion mechanism that starts at the bottom.
· Renewable Details: Seals, gaskets and fittings are individually renewable rather than requiring whole-roof work.
2. How Is Readiness Maintained During Storage?
By exercising the systems that must work on demand and by verifying condition without emptying the tank. Readiness is a maintenance discipline, not a design feature.
· Instrumentation Exercise: Gauges, valves and alarms are exercised so they work when needed.
· Pump and Transfer Readiness: Transfer equipment is tested on schedule.
· Seal and Fitting Checks: Condition is inspected externally and recorded.
· Product Quality Checks: Periodic sampling confirms the stored product is still serviceable.
· Documentation: A clear readiness record supports rapid decision-making when the reserve is called.
3. What Inspection Regime Suits Reserve Duty?
One that maximises what can be done in service and minimises what requires emptying. Corrosion monitoring, external inspection and coating and protection surveys carry most of the load.
· In-Service Monitoring: Corrosion rate monitoring, cathodic protection surveys and external inspection.
· Non-Entry Techniques: Where applicable, examination methods that do not require emptying reduce outage frequency.
· Planned Internal Examination: Full internal inspection is scheduled long in advance and coordinated with the reserve's availability.
· Trend Records: Readings are trended so remaining life can be predicted rather than guessed.
· Spares Philosophy: Critical seals, gaskets and fittings are held so repairs are not waiting on procurement.
Evaluation Criterion | Reserve-Duty Design | Commercial Terminal Design |
Corrosion allowance basis | Full design life | Typical commercial interval |
Inspection without emptying | Maximised | Standard |
Readiness regime | Exercised and documented | Implicit |
Renewable details | Individually renewable | Whole-component renewal |
Spares philosophy | Critical spares held | Procured as needed |
Engineering Assurance and Project Support
Every welded oil tank delivered by Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel) is designed to API 650 with shell courses sized by the one-foot method and checked for wind, seismic and hydrostatic load cases, or to EN 14015 and the Eurocodes where the site is European. Shell plate is shot-blasted to Sa 2.5 and coated to a documented dry film thickness, longitudinal and annular plate welds are examined by radiography or ultrasonic testing to the acceptance level written into the purchase order, and every tank is hydrostatically tested and dimensionally surveyed before hand-over. Reserve tanks are supplied with long-life coating and cathodic protection, water management, in-service monitoring provisions, a documented readiness regime and a critical spares recommendation.
Frequently Asked Questions (FAQ)
How long can an oil reserve tank stay in service?
Several decades is a normal design expectation when corrosion allowance, coating, cathodic protection and water management are specified together and the tank is monitored. The limit is usually reached through a component that was not designed for the life - a coating system, a seal or instrumentation - rather than through the shell itself.
How do you inspect a tank that cannot easily be taken out of service?
By maximising what can be done in service: corrosion rate monitoring, cathodic protection surveys, external inspection, seal and fitting checks and product sampling. Full internal examination is then scheduled long in advance. Non-entry examination techniques, where applicable, further reduce how often emptying is needed.
Does stored crude degrade over long periods?
It can. Lighter fractions are retained if the tank has vapour control, but water bottoms, sediment and microbial activity can still affect quality. Periodic sampling and routine water draw-off are what confirm the product is still serviceable when the reserve is called forward.
Can the tank be customised for our reserve programme?
Yes. Capacity and geometry, corrosion allowance, coating and cathodic protection, roof and seal specification, water management, monitoring instrumentation, access provisions and a spares recommendation are all engineered to your product, site and availability requirements.