Biogas Holders For Biological Wastewater Treatment Plants: Energy Recovery And Safe Containment
A wastewater treatment plant produces biogas as a by-product of sludge digestion, and the gas is the plant’s only significant energy asset. The holder between the digesters and the utilization equipment decides how much of that asset is actually recovered — and the integration into the treatment train is where the design is won or lost.
This article covers biogas holders for biological wastewater treatment plants: the digester gas profile, the integration into the treatment train, the safety systems and the energy recovery outcome.
Sludge Digester Gas Profile
Digester gas production follows the sludge loading, which follows the plant’s influent and its treatment configuration. The daily profile is comparatively steady — digesters are buffered biological systems — but it moves seasonally with load and temperature.
The profile also carries the upset cases: a digester upset drops production sharply, and a feeding surge raises it. The holder sizing covers both, because the energy recovery equipment keeps running through both.
Holder Role In The Treatment Train
The holder sits between the digester gas outlet and the utilization equipment, with the gas cleanup — dewatering and desulphurisation — in between. Its role is to decouple the production from the consumption so the utilization equipment runs at its design condition.
The holder is also the safety buffer for the digester itself: it absorbs the gas when the utilization stops, protecting the digester from overpressure and keeping the biological process stable through the downstream outage.
Storage Volume For WWTP Duty
The WWTP storage volume is sized from the digester production against the utilization consumption, carrying the planned maintenance outages and the upset production swings. The plant’s operating pattern — continuous base-load CHP or daytime boiler duty — sets the shape of the requirement.
The sizing also covers the digester protection case: the volume the holder must absorb when the utilization equipment stops unexpectedly, because the digesters keep producing until the process is adjusted.
Sizing Input | WWTP Consideration | Design Note |
Digester gas production | Seasonal load and temperature variation | Sets the base storage turnover |
Utilization consumption rate | CHP or boiler design capacity | Sets the drawdown rate |
Planned outage allowance | Utilization maintenance schedule | Sets the outage storage volume |
Digester protection case | Gas production during utilization stop | Sets the emergency absorption volume |
Pressure Control And Gas Piping
The pressure control holds the digester gas space at its design pressure while the holder inventory changes. The control coordinates the digester backpressure with the blower duty, because the digester has its own pressure limits that must not be exceeded.
The gas piping is part of the control design: the line sizes, the slope and the low-point drains keep the wet gas moving and the condensate out of the blower, and the isolation valves allow a section to be worked without shutting the train.
Safety Systems And Interlocks
The safety set covers the digester protection, the holder protection and the utilization protection. The digester relief protects the biological asset; the holder relief protects the storage; the interlocks stop the train when a parameter leaves its band.
The interlocks are the integration’s safety layer: the holder level, the blower state and the utilization state are cross-connected so no single equipment decision can push the digester or the holder outside its design envelope.
Odor And Emission Control
WWTP gas handling is an odour management exercise as much as an energy one. The digester gas is saturated and sulphurous, and every vent, leak and relief discharge is a potential odour source that the plant’s neighbours will notice.
The emission control covers the relief discharge routing — to a flare or a scrubber rather than the atmosphere — the leak-tight gas path specification and the enclosed holder arrangement where the site sensitivity requires it.
Corrosion In Digester Gas Service
Digester gas attacks the gas train in the wet phase. The H2S in contact with the condensate corrodes the pipework, the blower internals and the holder’s metal components, and the corrosion rate follows the H2S concentration and the wetness.
The design answers with material selection in the wet zones, condensate drainage that keeps the surfaces dry, and the gas cleanup upstream that removes the H2S before it reaches the storage.
Component | Corrosion Exposure | Design Response |
Gas piping | Wet H2S gas at line temperature | Material selection and sloped runs to drains |
Blower internals | Condensate and H2S contact | Material selection and drain upstream |
Holder metal components | Vapour phase H2S and moisture | Protected or stainless components |
Low points and traps | Condensate accumulation | Accessible drains with service schedule |
Retrofit On Existing WWTPs
Most WWTP holder projects are retrofits onto an existing digester and gas train. The retrofit design starts from the existing digester pressure limits, the existing gas piping and the existing utilization equipment, and the holder has to fit that envelope.
The retrofit also manages the live plant: the tie-in sequence, the isolation points and the commissioning windows are planned around the treatment process, which cannot be shut down for the work.
Monitoring And Operations
The monitoring set covers the gas train: digester pressure, holder level and pressure, blower duty, gas quality and the utilization equipment state. The operations team runs the train from these readings, and the trends show the energy performance.
The operating discipline covers the condensate drains, the relief device checks and the leak survey — the routine tasks that keep the train efficient, scheduled from the operating record rather than the calendar.
Energy Recovery Integration
The energy recovery outcome is what the holder design serves. The CHP engine or the boiler needs gas at a stable pressure and a clean composition, and the holder and its control deliver that condition across the production variability.
The integration also covers the heat recovery: the engine jacket water and exhaust heat serve the digester heating, closing the energy loop that makes the WWTP biogas project pay for itself.
Center Enamel WWTP Holder Delivery
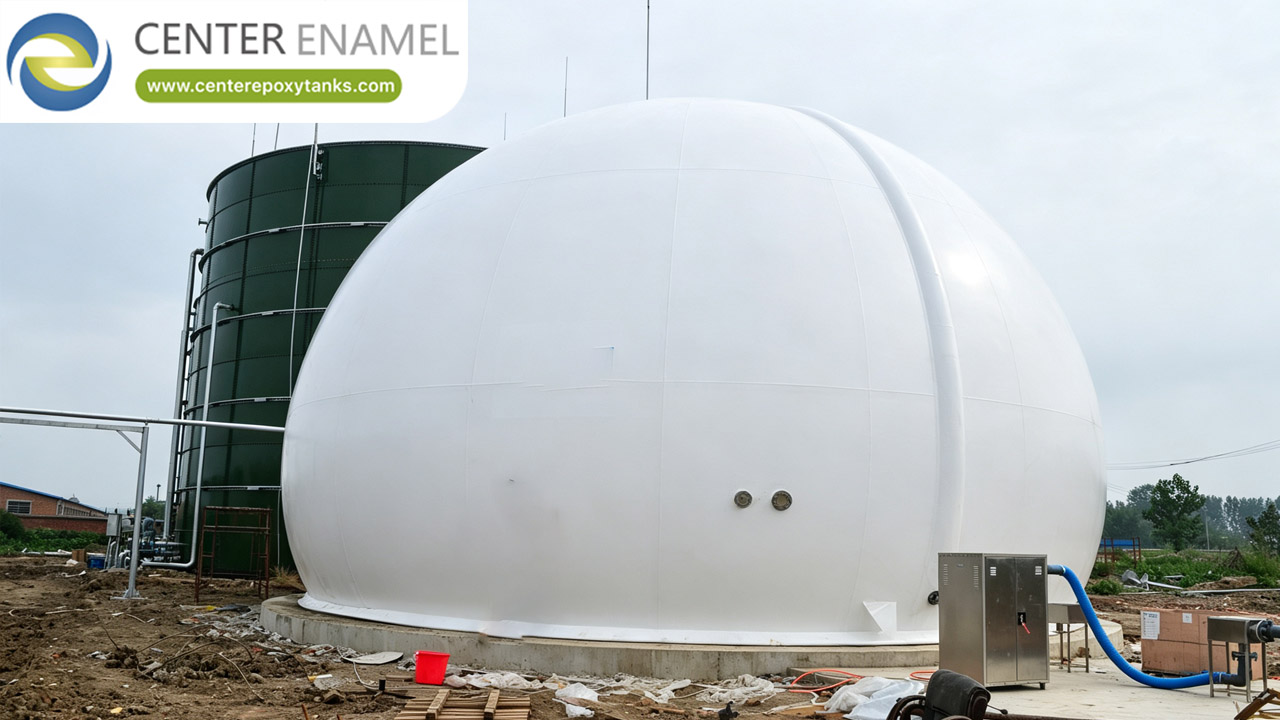
Center Enamel delivers biogas holders for wastewater treatment plants with the gas containment engineering, safety interlocks and retrofit integration that live-plant projects require. The delivery covers the holder, the control and safety scope and the commissioning support.
Our engineering team supports holder sizing and retrofit integration against the existing digester and gas train. Contact our engineering team for WWTP biogas holder procurement guidance on your next project.
Project Case Study
A food waste digestion project in Sichuan, China required digestion capacity in a modular configuration matched to the plant’s commissioning sequence. Center Enamel supplied four glass-fused-to-steel bolted tanks at 5.35 m diameter by 7.2 m height each, totaling 648 m3, configured for the digestion duty.
The four-tank configuration staged the digestion capacity against the plant’s ramp-up rather than committing the full volume at once, with the vitreous enamel interior carrying the digester chemistry across every unit. The project was delivered and completed in August 2025.
Project Reference | 01 China Sichuan Food Waste 202508 |
Location | China |
Application | Food Waste |
Product / Technology | Glass-Fused-to-Steel (GFS) Bolted Tank |
Tank Count | 4 |
Tank Dimensions | φ5.35*7.2m(H), 4 units |
Total Volume | 648 m3 |
Completion | Delivered and completed 2025-08 |
Supply Scope Note | B relevance grade to this topic |
About Company
Shijiazhuang Zhengzhong Technology Co.,Ltd(Center Enamel) is a professional manufacturer dedicated to the design and fabrication of bolted storage tanks since 2008. Our products range includes Glass-Fused-to-Steel (GFS) tanks, fusion bonded epoxy tanks, stainless steel tanks, galvanized steel tanks and aluminum geodesic dome roofs. With professional enameling R&D team and nearly 200 enameling patents, Shijiazhuang Zhengzhong Technology Co.,Ltd has become the leader in bolted tanks industry of Asia. Our products are certified to ISO9001, NSF61, EN1090, ISO28765, WRAS ,FM, LFGB, BSCI, IS0 45001 and other international standards.
Shijiazhuang Zhengzhong Technology Co., Ltd is not only the first manufacturer in China which produces Glass-Fused-to-Steel tanks, but also the most experienced professional bolted tanks manufacturer in Asia.The engineering & design, product testing and quality system of Center Enamel Glass-Fused-to-Steel tanks is in strict accordance with AWWA D103-09, OSHA, ISO 28765, NSF/ANSI 61, NFPA and other international standards. Until 2023, Center Enamel bolted tanks have been exported to more than 100 countries including USA, Australia,Canada, Malaysia, Indonesia, Russia, UAE, Panama,Brazil and South Africa etc., the superior tank quality and prompt service gains us worldwide recognition.
As an outstanding containment and cover system provider with decades of industry experience, Shijiazhuang Zhengzhong Technology Co., Ltd sincerely expects to establish long-term cooperation with the local partners throughout the world and make continuous contribution to the development of the industry.
Suggested CTA
Center Enamel delivers biogas holder engineered for wwtp biogas recovery duty, with wwtp project delivery, gas containment engineering. Contact our engineering team for engineering guidance on your next biogas holder wastewater treatment plant project — including sizing, standards compliance and delivery scheduling.
Frequently Asked Questions
Q: Where does WWTP biogas come from?
A: From the anaerobic digestion of the sludge the treatment process produces. The gas yield follows the sludge loading, which follows the influent flow and the treatment configuration, with seasonal variation from load and temperature.
Q: What role does the holder play in the treatment train?
A: It decouples digester production from utilization consumption so the CHP or boiler runs at its design condition, and it protects the digester by absorbing gas when the utilization equipment stops unexpectedly.
Q: How is WWTP holder storage volume sized?
A: From digester production against utilization consumption, carrying the planned outage allowance and the digester protection case — the volume absorbed when utilization stops and the digesters keep producing.
Q: What safety interlocks does a WWTP gas train need?
A: Cross-connection of holder level, blower state and utilization state so no single equipment decision pushes the digester or holder outside its design envelope, plus digester relief protecting the biological asset.
Q: How is odour controlled on a WWTP gas holder?
A: Relief discharges route to a flare or scrubber rather than atmosphere, the gas path is specified leak-tight, and the holder is arranged enclosed where the site sensitivity requires it.
Q: Why choose Center Enamel for WWTP biogas holders?
A: Center Enamel delivers biogas holders with gas containment engineering, safety interlocks and retrofit integration for live-plant projects. Contact our engineering team for procurement guidance.