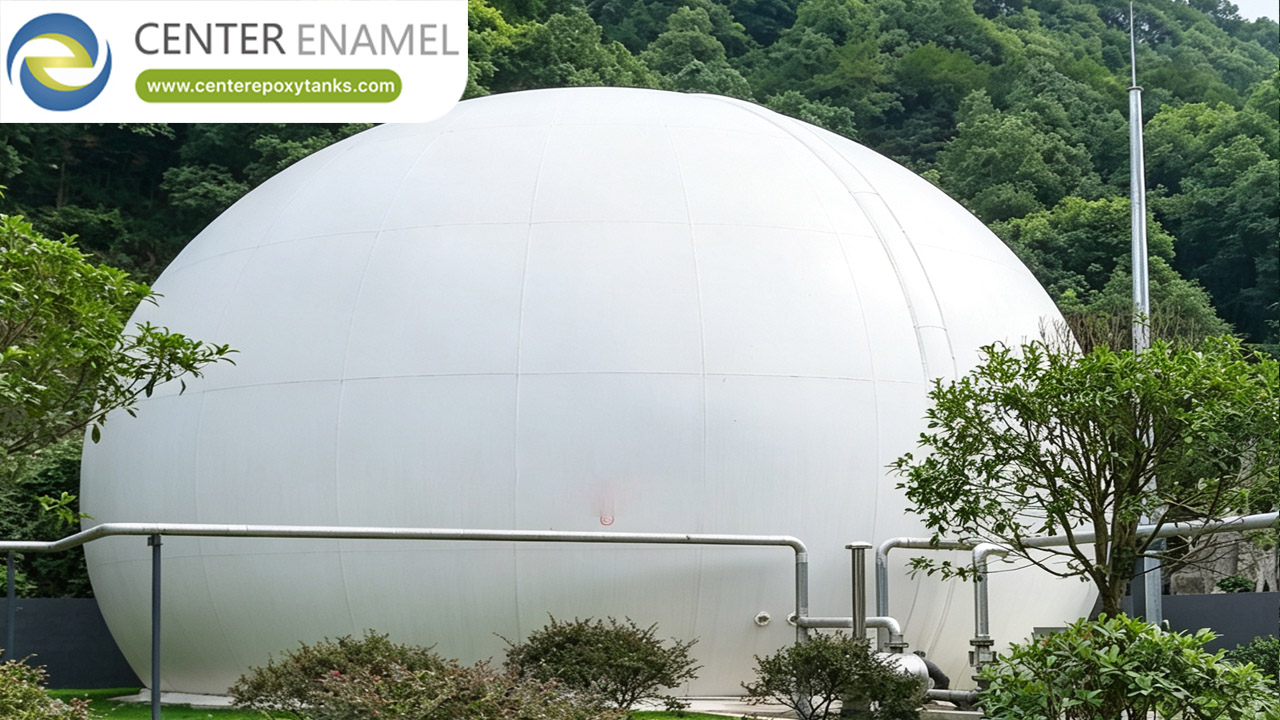
Biogas Holder Design For High-Efficiency Gas Storage: Engineering Energy Recovery
Gas storage is usually specified as a volume and a pressure. High-efficiency storage is specified as a loss budget: every millibar of pressure instability, every leak path and every condensate trap removes gas from the energy recovery train that the plant paid to produce. The holder design decides how much of the production actually reaches the utilization equipment.
This article covers biogas holder design for high-efficiency gas storage: the loss mechanisms to design out, the volume and pressure optimization, and the integration with energy recovery equipment.
Efficiency In Gas Storage Terms
Storage efficiency is measured in delivered gas, not in tank terms. The metric is the fraction of produced gas that reaches the utilization equipment at usable pressure — and the losses between production and utilization are what the holder design controls.
The loss budget has four entries: leakage, pressure-driven venting, condensate carryover that blocks downstream equipment, and flaring from buffer exhaustion. Each is a design and control problem with a known answer.
Loss Mechanisms To Design Out
Leakage is the silent loss. The gas path — connections, seals, valve stems, membrane penetrations — all leak a little, and the design answer is the leak-tight specification, the joint discipline and the periodic leak survey that finds the paths before they grow.
Pressure-driven venting is the controlled loss. The relief and vent set points trade safety against loss, and the design sets them from the actual operating band rather than a conservative default that vents good gas.
Volume Optimization
Volume optimization sizes the buffer against the actual production and consumption curves rather than rules of thumb. The oversized buffer costs capital and holds stale gas; the undersized one flares at every production peak. The optimization is the curve analysis.
The optimization also covers the working volume: the level band the control actually uses, above the dead volume the blower cannot reach and below the relief set point, is what the sizing must cover.
Design Lever | Efficiency Effect | Trade-off |
Buffer volume right-sizing | Reduces flaring at production peaks | Capital cost of the additional volume |
Tight pressure control band | Stable delivery to utilization | Control system complexity and response speed |
Leak-tight gas path specification | Reduces silent inventory loss | Joint and seal specification cost |
Condensate drainage design | Protects downstream equipment uptime | Additional low points and drain scope |
Pressure Control Precision
Pressure precision is what the utilization equipment actually experiences. A CHP engine tolerates a band; an upgrading membrane does not — and the control design matches the band to the equipment, with the response speed the band requires.
The precision comes from the control loop and the actuator sizing together: the sensor range and accuracy, the control algorithm and the blower or valve response all have to deliver the band, not just measure it.
Energy Recovery Interfaces
The interface with the energy recovery equipment is a pressure and flow contract. The holder and its blower set deliver gas at the pressure and flow the equipment requires across its operating range, and the control coordinates the two so neither starves the other.
The interface also covers the shutdown states: when the recovery equipment stops, the storage must absorb the production rather than flare it, and the control logic makes that transition without operator intervention.
Thermal And Condensate Management
Biogas is saturated, and every temperature drop condenses water in the gas path. The condensate blocks pipes, corrodes vessels and blinds the downstream filters — so the thermal design keeps the gas above its dew point where it can and drains where it cannot.
The drainage design is geometry: low points at every pocket, sloped runs, accessible traps and the drain schedule that keeps them clear. It is the least glamorous part of the design and one of the most valuable.
Monitoring And Leakage Control
The monitoring set covers the efficiency metrics, not just the safety ones: pressure, volume, flow at both ends of the storage and the derived inventory balance. The balance between production and delivery is the leakage indicator.
The leakage control programme runs on the monitoring: a scheduled leak survey of the gas path with the findings tracked, so the leak population is managed as a maintenance backlog rather than discovered as an inventory shortfall.
Membrane Versus Rigid For Efficiency
The format choice has efficiency consequences. Membrane holders have no internal mechanism to leak and no gas space corrosion, but their pressure band is limited and the membrane itself is a diffusion boundary; rigid holders hold pressure better but add seals, corrosion surfaces and inspection scope.
The selection follows the pressure requirement and the gas cleanliness: where the utilization demands a stable elevated band, the rigid format or a compression stage earns its cost; where the band is low and the gas is treated, the membrane format wins on simplicity.
Aspect | Membrane Holder | Rigid Holder |
Leak paths | Penetrations and seams only | Seals, valves and corrosion surfaces |
Pressure band | Low band with blower support | Elevated band without compression |
Gas space corrosion | None with compatible membrane | Material selection or protection required |
Inspection scope | Visual membrane inspection | Internal inspection at shutdowns |
Control Philosophy
The control philosophy states what the system does in every state: normal operation, production peak, utilization outage, control failure. Each state has a defined storage behaviour, and the design proves the behaviour rather than assuming it.
The philosophy also covers the handover to manual: the operator override path, the mechanical protection that remains active and the flare as the last-resort sink are all part of the design, not afterthoughts.
Commissioning For Efficiency
Commissioning verifies the efficiency claims, not just the safety interlocks. The pressure band is proven under real production, the leakage rate is measured against the inventory balance, and the control transitions are exercised across the operating states.
The commissioning data becomes the baseline: the efficiency metrics recorded at handover are what the operations team compares against, so degradation is visible as a trend rather than a surprise.
Center Enamel High-Efficiency Holder Engineering
Center Enamel engineers high-efficiency biogas holders with the volume optimization, pressure control and leakage discipline that energy recovery duty demands. The engineering covers the holder, the control scope and the commissioning verification.
Our engineering team supports holder sizing and control design against the production profile and the recovery equipment. Contact our engineering team for high-efficiency holder design and procurement guidance.
About Company
Shijiazhuang Zhengzhong Technology Co.,Ltd(Center Enamel) is a professional manufacturer dedicated to the design and fabrication of bolted storage tanks since 2008. Our products range includes Glass-Fused-to-Steel (GFS) tanks, fusion bonded epoxy tanks, stainless steel tanks, galvanized steel tanks and aluminum geodesic dome roofs. With professional enameling R&D team and nearly 200 enameling patents, Shijiazhuang Zhengzhong Technology Co.,Ltd has become the leader in bolted tanks industry of Asia. Our products are certified to ISO9001, NSF61, EN1090, ISO28765, WRAS ,FM, LFGB, BSCI, IS0 45001 and other international standards.
Shijiazhuang Zhengzhong Technology Co., Ltd is not only the first manufacturer in China which produces Glass-Fused-to-Steel tanks, but also the most experienced professional bolted tanks manufacturer in Asia.The engineering & design, product testing and quality system of Center Enamel Glass-Fused-to-Steel tanks is in strict accordance with AWWA D103-09, OSHA, ISO 28765, NSF/ANSI 61, NFPA and other international standards. Until 2023, Center Enamel bolted tanks have been exported to more than 100 countries including USA, Australia,Canada, Malaysia, Indonesia, Russia, UAE, Panama,Brazil and South Africa etc., the superior tank quality and prompt service gains us worldwide recognition.
As an outstanding containment and cover system provider with decades of industry experience, Shijiazhuang Zhengzhong Technology Co., Ltd sincerely expects to establish long-term cooperation with the local partners throughout the world and make continuous contribution to the development of the industry.
Suggested CTA
Center Enamel delivers biogas holder engineered for biogas storage duty, with holder design engineering, energy recovery integration. Contact our engineering team for engineering guidance on your next biogas holder design project — including sizing, standards compliance and delivery scheduling.
Frequently Asked Questions
Q: What makes biogas gas storage efficient?
A: Delivering the maximum fraction of produced gas to the utilization equipment at usable pressure. The levers are buffer volume right-sizing, tight pressure control, a leak-tight gas path and condensate management that protects downstream uptime.
Q: How is buffer volume optimized?
A: By sizing against the actual production and consumption curves rather than rules of thumb. The working volume must cover the level band the control uses, above the blower dead volume and below the relief set point.
Q: Why does pressure precision matter for energy recovery?
A: CHP engines tolerate a band; upgrading membranes do not. The control design matches the pressure band to the equipment with the response speed the band requires, so the recovery equipment runs at its design condition.
Q: How is storage leakage controlled?
A: With a leak-tight gas path specification, scheduled leak surveys tracked as a maintenance backlog, and an inventory balance between production and delivery flows that reveals losses as a trend rather than a shortfall.
Q: What is the role of condensate management in efficiency?
A: Condensate blocks pipes, corrodes vessels and blinds downstream filters. The thermal design keeps gas above its dew point where possible and drains where not, with sloped runs, accessible low points and a drain schedule.
Q: Why choose Center Enamel for high-efficiency holder design?
A: Center Enamel engineers biogas holders with volume optimization, pressure control precision and leakage discipline for energy recovery duty. Contact our engineering team for holder design and procurement guidance.


