Tank Coating & Powder Coating Protection: Comparing Modern Lining Systems
The most expensive tank decision is almost never the steel — it is the coating that fails. Every lining system on the market is a different bet on how to keep water, chemicals, and fuel away from carbon steel for 20 to 40 years, and each chemistry wins under different conditions. Choosing by purchase price alone is how a five-year recoat project begins.
Tank coating and powder coating protection encompasses the engineered barrier systems applied to steel storage tanks: fusion bonded epoxy (FBE) powder linings at 300-500 microns, Glass-Fused-to-Steel (GFS) coatings fired at 820-930 deg C, and hot-dip zinc systems — each applied over SSPC-SP10-class surface preparation and verified by holiday testing before service.
1. How Do Liquid Epoxy and Powder Coating Systems Differ?
Application physics drives the performance gap between liquid and powder systems.
· Liquid epoxy linings: Two-component epoxies sprayed and cured on site or in-shop; versatile and repairable, but film build, cure windows, and ambient humidity inject variability into every coat.
· Fusion bonded epoxy (FBE): Thermoset powder electrostatically applied to preheated blast-cleaned plate and oven-cured; single-bake polymerization delivers uniform 300-500 micron films with near-zero solvent entrapment.
· Surface preparation discipline: Both systems depend on SSPC-SP10 near-white blast cleanliness; powder systems control it in the factory, removing weather from the quality equation entirely.
· Testing regime: 1,500 V (GFS and heavy FBE) or 1,100-900 V spark testing verifies film continuity panel by panel before a tank is even shipped.
2. What Makes Glass-Fused-to-Steel the Benchmark Lining?
GFS is not a coating applied to steel — it is a material created with steel.
· Ceramic bond: Glass frit melts into the steel surface at 820-930 deg C, creating adhesion of 3,450 N/cm2 that no organic coating approaches.
· Inert service face: The vitreous surface is chemically inert, smooth, and anti-adhesive, shrugging off pH 1-14 in special formulations and biofilm formation in digesters.
· Hardness and abrasion: 6.0 Mohs hardness survives sludge contact and aggressive cleaning that abrades organic films.
· Proven longevity: 30+ year service life with no recoating cycle is documented across bolted tanks in 100+ countries.
3. Which Coating Fits Which Duty?
A duty-matched matrix beats a one-system-fits-all specification every time.
· Potable water: NSF/ANSI 61-listed GFS or epoxy systems — factory-applied and certified.
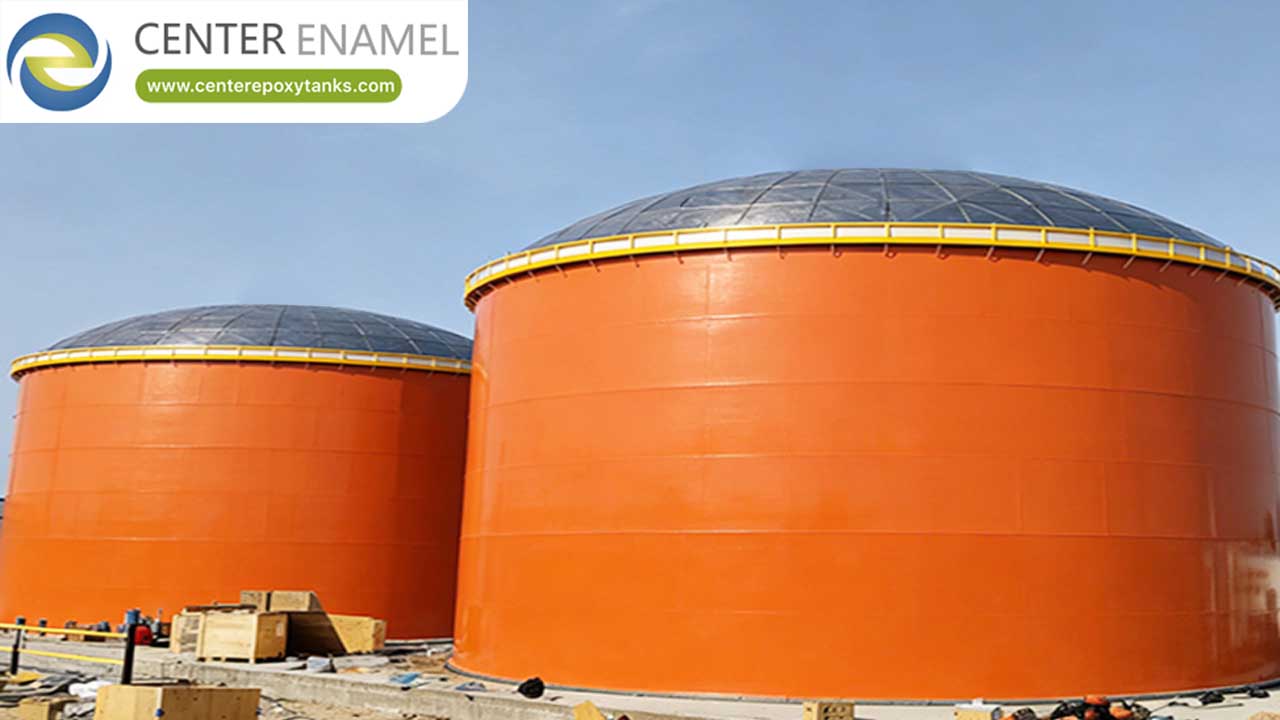
· Municipal and industrial wastewater: GFS (2C2F/3C3F grades for aggressive streams) or heavy FBE; a 2 x 6,578 m3 epoxy bolted installation at a Chilean desalination plant (2025) shows FBE's seawater capability.
· Fire and irrigation water: Hot-dip galvanizing where water is mild and budgets tight.
· Fuel and oil service: Tank-bottom and internal epoxy phenolic or FBE systems rated for hydrocarbon immersion; exterior zinc-epoxy-PU weathercoats.
Data Table: Tank Coating Systems Compared
Property | GFS (Glass-Fused) | FBE Powder | Liquid Epoxy | Hot-Dip Zinc |
Film thickness | 0.25-0.45 mm | 300-500 microns | 250-500 microns | 85-100+ microns |
Application | Factory firing 820-930 deg C | Factory bake | Shop or site spray | Molten dip ~450 deg C |
Adhesion | 3,450 N/cm2 | Excellent | Good | Metallurgical bond |
Chemical range | pH 1-14 special | pH 2-11 | System-dependent | ~pH 6-12 immersion |
Service life | 30+ years | 20-25 years | 15-20 years | 20+ years (mild water) |
Relative cost | Medium-high | Medium | Low-medium | Low |
Frequently Asked Questions (FAQ)
Q1: What is the best coating for a steel water tank?
For potable and aggressive water, Glass-Fused-to-Steel is the benchmark — a ceramic layer fired at 820-930 deg C with 3,450 N/cm2 adhesion and 30+ year life. For chemical and seawater duties, fusion bonded epoxy at 300-500 microns is highly capable, while hot-dip zinc suits mild fire and irrigation service at the lowest cost.
Q2: How does powder coating protect tanks better than liquid paint?
Powder systems — FBE for linings, polyurethane powders for exteriors — cure in one bake cycle with no solvents, giving pinhole-free, uniform films applied and tested indoors. Site-applied liquid coatings inherit weather, humidity, and applicator variability; factory powder systems eliminate those variables and are spark-tested panel by panel.
Q3: What is a holiday test on tank coatings?
A high-voltage spark test (typically 1,500 V for GFS and heavy FBE films) that sweeps the coating surface to detect any discontinuity or pinhole — a 'holiday' — before the tank enters service. Factory holiday testing is a core reason bolted, factory-coated tanks outperform field-coated welded shells.
Q4: How often do tank coatings need recoating?
GFS linings typically never require interior recoating in a 30+ year life; FBE systems run 20-25 years; liquid epoxies often need maintenance at 15-20 years. Exterior weathercoats are inspected every few years and touched up as needed — a fraction of interior recoat cost.