Petroleum Storage Tanks: Advanced Engineering For Safe Hydrocarbon Containment
Once the basics of petroleum storage are settled, the engineering depth lives in three places: the shell, the atmosphere above the product, and the weld that joins the plates. This article is written for engineers and owner’s representatives who already know what a tank is and need the design logic behind it — how shell courses are actually sized, how wind and seismic load cases are applied, how corrosion allowance is budgeted, and how breathing and emission control are engineered.
The thread connecting all of it is verification. Every value on a tank drawing is a claim that a downstream inspection regime must be able to prove.
Shell Course Design Logic
A vertical cylindrical tank shell is a stack of courses, each thicker toward the bottom because hydrostatic pressure rises linearly with product depth. API 650 provides two design methods: the one-foot method, which calculates required thickness at discrete elevations, and the variable-design-point method, which optimizes course boundaries for minimum steel. The design pressure itself is modest — near atmospheric — so the shell is usually governed by hydrostatic test conditions, wind buckling, or seismic overturning rather than operating pressure.
For bolted configurations, the logic inverts: standard panel gauges are selected from a catalog of stamped thicknesses, and the engineer chooses the course layout that satisfies the load cases with available panel types. This is why bolted tank engineering is fast but bounded — the catalog is the design space.
Wind And Seismic Load Cases
Wind acts on a tank in three ways: external pressure that can buckle the upper shell, internal suction during emptying that can buckle the same courses from inside, and overturning that lifts the shell edge on the windward side. API 650 Annex E and F formalize seismic detailing: shell compression resistance, anchorage, and the interaction of uplift with foundation hold-down. A tank designed without these annexes is not seismically qualified regardless of its nameplate.
The uplift case is the one that surprises owners. When internal pressure from wind suction and product movement combine to exceed the shell’s weight, the tank must be anchored — and the foundation must be designed for the anchor forces, not just the bearing load.
Corrosion Allowance Budgeting
Corrosion allowance is a consumable budget drawn against the tank’s service life. Typical values for wetted carbon steel surfaces in hydrocarbon service run 1.6 mm to 3.2 mm, sized from the expected corrosion rate and the inspection interval. The allowance is spent at the rate the environment dictates, and the integrity program exists to measure the remaining balance before it reaches zero.
Coatings change the economics, not the physics. An FBE internal coating at 400-800 microns does not eliminate allowance; it extends the interval over which the allowance is consumed. The engineering discipline is to size both together — coating for the credible environment, allowance for the credible uncertainty.
Service Environment | Typical Corrosion Allowance | Coating System | Inspection Interval |
Refined products (gasoline, diesel) | 1.6 mm | FBE 400-800 microns | 5 years (UT thickness) |
Crude oil (sweet) | 2.0-3.2 mm | FBE or GFS panels | 3-5 years |
Crude oil (sour) | 3.2 mm+ | FBE plus bottom reinforcement | 3 years |
Wastewater / sludge | 2.0-3.2 mm | GFS or FBE, splash zone detailed | 3-5 years |
Chemical / solvent | Material-dependent | Stainless or lined | Per RBI program |
Breathing, Venting And Emission Control
Every fixed-roof tank exchanges vapor with the atmosphere: pumping out displaces air in (inbreathing), filling and thermal expansion push vapor out (outbreathing). Vents are sized for the maximum credible rates in both directions, with flame arrestors specified for the product group. Under-sizing vents manifests as shell distortion under pump-out — a structural failure caused by a fitting.
Emission control goes further: internal floating roofs, vapor recovery systems and closed vent headers are all responses to the standing-loss and working-loss problem. The choice among them is an economics decision driven by product value, local regulation and the terminal’s recovery infrastructure.
Welding Qualification And NDT Regimes
API 650 ties weld quality to procedure qualification records and welder performance qualifications — the documentation that proves a given joint can be produced repeatably. Radiographic or ultrasonic examination is applied to full-penetration welds in the shell bottom and to specified percentages of shell and roof seams, with acceptance criteria per the code.
The practical lesson for buyers: ask for the welding procedure specifications and the NDT coverage map, not just the code reference. A tank welded under qualified procedures with 10 percent RT on shell seams is a different asset from one with visual inspection only, even though both are "API 650 tanks".
Foundations And Settlement
Tank foundations are engineered for uniform bearing, because differential settlement stresses the shell non-uniformly. The classic failure mode is edge settlement on the windward side, which concentrates stress in the bottom courses. Ringwall foundations with controlled backfill and crushed-stone drainage beneath the bottom are the standard answer; leak detection under the bottom is increasingly specified as a second barrier.
Bolted tanks are more forgiving of minor differential movement because panel joints accommodate small rotations, but no tank tolerates poor soil. Geotechnical investigation is a design input, not a formality.
Roof Systems: Fixed, Floating, Internal
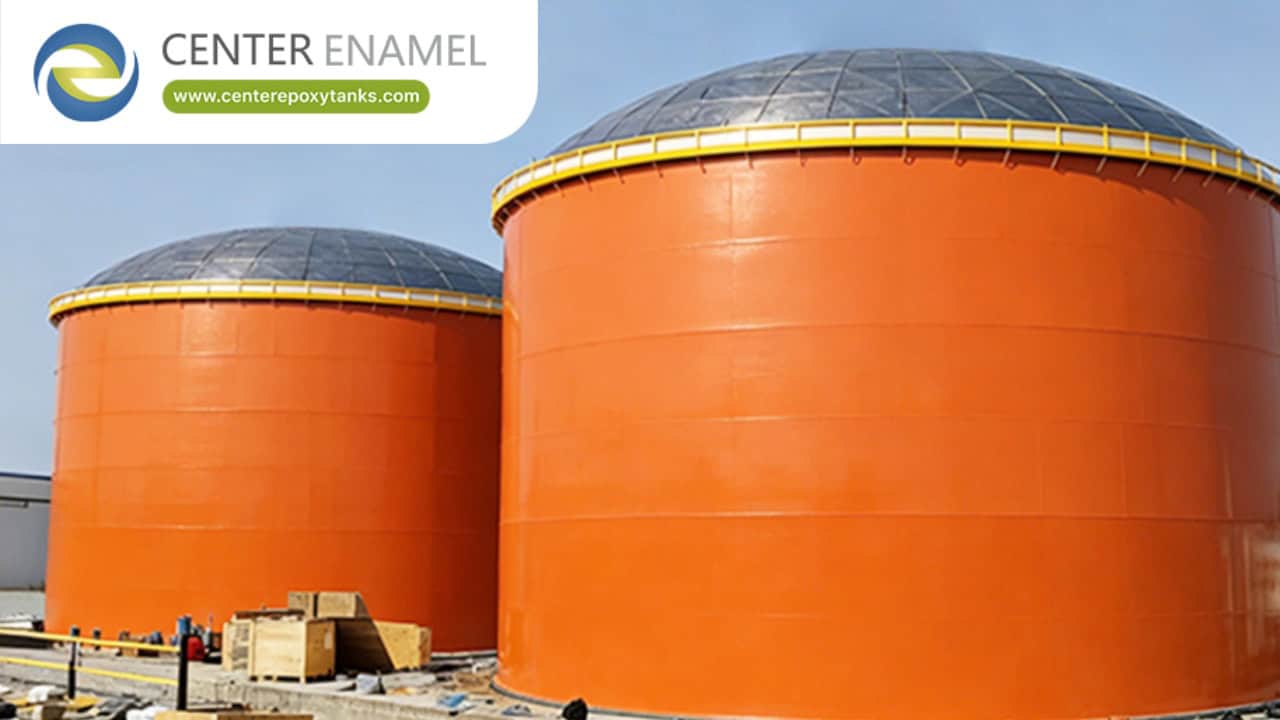
Roof selection is emission management plus structural design. Cone roofs are the default fixed solution; domed roofs — including aluminum geodesic systems — add clear span and drainage performance. External floating roofs serve volatile crude and product service directly; internal floating roofs retrofit vapor control into fixed-roof tanks at a fraction of replacement cost.
Each roof type carries its own detailing: pontoon sizing and drain systems for floating roofs, snow and wind load checks for domes, and sealed penetrations for all. Roof drains that fail during a storm have taken down more tanks than design pressure ever has.
Roof Type | Vapor Control | Best-Fit Duty | Key Design Check |
Fixed cone roof | Breathing venting only | Non-volatile products | Vent sizing for pump-out |
Dom roof (steel or aluminum geodesic) | Breathing venting | Large-diameter water and product tanks | Clear span, snow and wind load |
External floating roof | Direct product contact | Volatile crude and products | Pontoon sizing, drain system |
Internal floating roof | Retrofit into fixed roof | Emission-regulated volatile storage | Seals, supports, vent capacity |
Heating, Mixing And Product Conditioning
Heavy products — heavy fuel oil, bitumen, waxy crudes — require heating coils or external heaters to maintain pumpability, and mixing to homogenize temperature strata. Coil design must consider thermal expansion, steam condensate drainage and the corrosion environment under insulation. For tanks storing temperature-sensitive products, the heating regime is a product-quality system, not a utility.
Mixing systems — side-entry, top-entry or recirculation — are specified against the homogenization duty, not as a default fitting. Over-mixing heavy products can entrain water and light ends; under-mixing creates the temperature gradients the heating was installed to prevent.
Inspection Intervals And Integrity Programs
API 653 formalizes the inspection regime: external visual on a short interval, ultrasonic thickness mapping on a schedule set by measured corrosion rates, and internal inspection at code intervals or condition triggers. The corrosion allowance is the buffer that makes scheduling possible; the inspection program is the instrument that reads the buffer.
Digital tools have changed the practice: drone and robotic internal inspection, permanent thickness monitoring at known hot spots, and RBI (risk-based inspection) programs that concentrate internal entry on the tanks the data actually implicate.
Documentation That Survives The Handover
The deliverable that matters in year ten is the design and inspection dossier: calculations, weld maps, NDT reports, coating records, foundation data and the initial thickness baseline. Every future repair decision and every insurance negotiation references this file. A tank without it is an unknown asset, and unknown assets are discounted accordingly.
Center Enamel issues this documentation package as standard, including coating inspection records per panel and third-party inspection coordination where the owner requires it.
Center Enamel Engineering Execution
Our engineering team works to API 650, AWWA D103 and EN 14015 with ISO 9001 and EN 1090 execution discipline and a welding qualification program covering carbon steel, stainless and coated panel fabrication. For petroleum storage scopes we support specification review, coating verification and inspection coordination — whether the tank is our bolted system or a welded tank we are supporting as engineering partner.
The standard we hold ourselves to is simple: every number we issue must be verifiable by an inspector who was not in the room when it was decided.
About Company
Shijiazhuang Zhengzhong Technology Co.,Ltd(Center Enamel) is a professional manufacturer dedicated to the design and fabrication of bolted storage tanks since 2008. Our products range includes Glass-Fused-to-Steel (GFS) tanks, fusion bonded epoxy tanks, stainless steel tanks, galvanized steel tanks and aluminum geodesic dome roofs. With professional enameling R&D team and nearly 200 enameling patents, Shijiazhuang Zhengzhong Technology Co.,Ltd has become the leader in bolted tanks industry of Asia. Our products are certified to ISO9001, NSF61, EN1090, ISO28765, WRAS ,FM, LFGB, BSCI, IS0 45001 and other international standards.
Shijiazhuang Zhengzhong Technology Co., Ltd is not only the first manufacturer in China which produces Glass-Fused-to-Steel tanks, but also the most experienced professional bolted tanks manufacturer in Asia.The engineering & design, product testing and quality system of Center Enamel Glass-Fused-to-Steel tanks is in strict accordance with AWWA D103-09, OSHA, ISO 28765, NSF/ANSI 61, NFPA and other international standards. Until 2023, Center Enamel bolted tanks have been exported to more than 100 countries including USA, Australia,Canada, Malaysia, Indonesia, Russia, UAE, Panama,Brazil and South Africa etc., the superior tank quality and prompt service gains us worldwide recognition.
As an outstanding containment and cover system provider with decades of industry experience, Shijiazhuang Zhengzhong Technology Co., Ltd sincerely expects to establish long-term cooperation with the local partners throughout the world and make continuous contribution to the development of the industry.
Suggested CTA
Center Enamel delivers welded carbon steel engineered for crude and product storage duty, with in-house engineering team, iso 9001 and en 1090 execution, welding qualification. Contact our engineering team for engineering guidance on your next petroleum storage tanks project — including sizing, standards compliance and delivery scheduling.
Frequently Asked Questions
Q: What governs petroleum tank shell thickness design?
A: API 650 governs welded aboveground tanks via the one-foot method or variable-design-point method; EN 14015 is the European equivalent. The governing load case is usually hydrostatic test, wind buckling or seismic — not operating pressure, which is near atmospheric.
Q: What corrosion allowance is typical for hydrocarbon service?
A: 1.6 mm to 3.2 mm on wetted carbon steel surfaces, sized from the expected corrosion rate and the planned inspection interval. Coatings extend the interval over which the allowance is consumed; they do not remove the need for it.
Q: Why do tank vents need to be sized as a calculation?
A: Because inbreathing during pump-out can buckle the shell if the vent cannot admit air at the required rate, and outbreathing during filling can distort the roof or relief path. Vent sizing is a load case, not a fitting selection.
Q: What is the difference between external and internal floating roofs?
A: An external floating roof sits directly on the product as the tank’s primary roof; an internal floating roof is a floating deck inside a fixed-roof tank that eliminates the vapor space. Both reduce standing losses dramatically — internal roofs by 80-90 percent versus a bare cone roof.
Q: What NDT coverage should I require on shell welds?
A: Full-penetration bottom welds receive radiographic or ultrasonic examination per code; shell and roof seams receive a specified percentage — commonly 10 percent RT on vertical seams, with acceptance criteria per API 650. The coverage map should be a project document, not an assumption.
Q: How does seismic design affect tank cost?
A: Seismic detailing per API 650 Annex E/F adds shell stiffening, anchorage and foundation hold-down design. It is a modest percentage of tank cost but a major percentage of foundation cost — and omitting it renders the tank non-compliant in seismic zones regardless of nameplate.