Drilling Fluids Tank: Storing Mud and Brine on a Rig
Refineries, terminals, and processors across drilling and workover rigs face the same pressure: store drilling fluid (mud and brine) safely, satisfy tightening emission and safety rules, and keep the tank in service for decades. A roof that vents, a coating that blisters, or a seam that weeps turns a storage asset into a compliance liability and a maintenance sink.
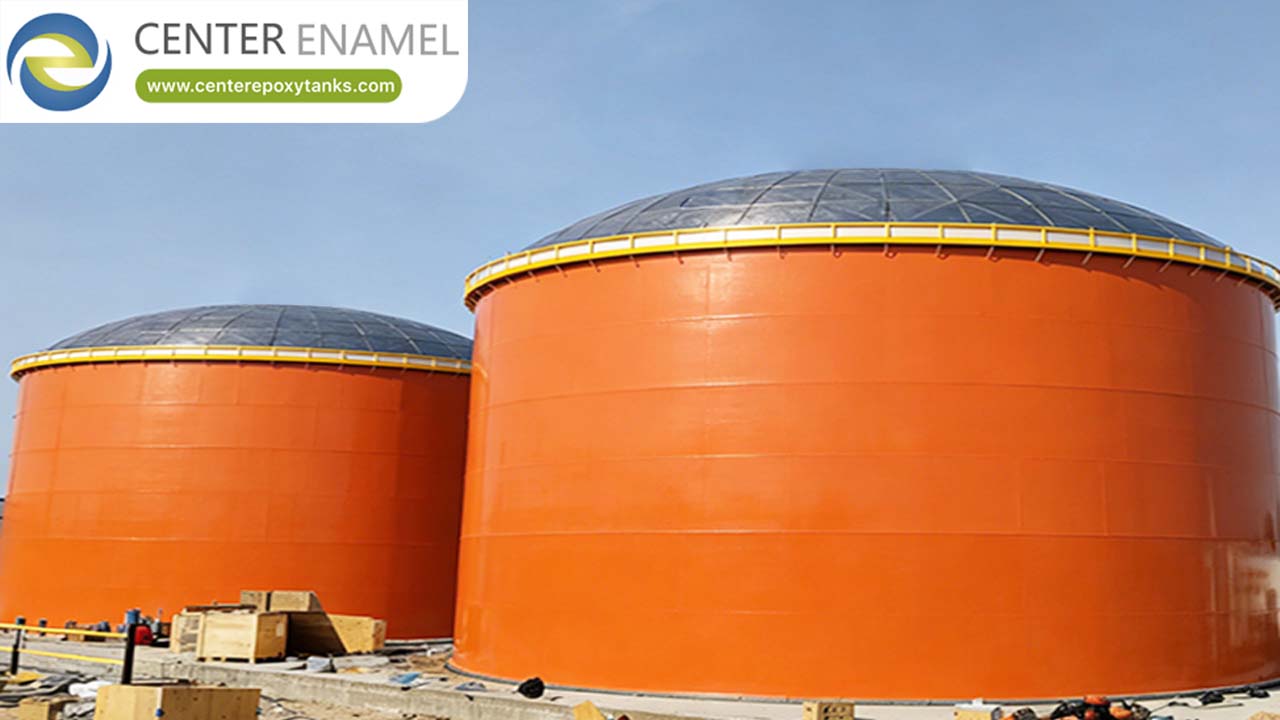
Engineered by Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel), a welded carbon steel tank pairs code-based structure with a coating and inspection regime built for oilfield fluid duty. The result meets API 650 and API 12F and keeps its margin through thermal cycles, fill-and-draw, and corrosive service.
1. What a carbon steel drilling fluid (mud and brine) Tank Is Built to Deliver
A carbon steel tank stores drilling fluid (mud and brine) under conditions where the wrong material or joint fails silently. The specification must answer corrosion, vapor, and structural load before a plate is cut, because drilling fluid (mud and brine) duty leaves no margin for a coating that quits or a seam that weeps, with 30-50 years of service life at stake.
· Service fit: Stores drilling fluid (mud and brine) where oilfield fluid duty drives the whole specification, from shell plate to roof and fittings.
· Structural basis: welded and skid-mounted to API 650 principles with the shell sized by the one-foot method where welded, or by course rating where bolted, then checked for wind and seismic load.
· Capacity: Single tanks span 20-5,000 m3, so one vessel can carry a terminal's daily throughput.
· Contents: Water-based or oil-based mud and brine are held for circulation, weighting, and disposal.
· Why it matters: The tank is the buffer between a volatile inventory and the atmosphere; its margin is the plant's margin.
2. Material, Coating, and Code
Material choice decides how the tank resists the product and the environment. carbon steel is selected for oilfield fluid duty, then protected by surface preparation and a coating system verified to 0.25-0.40 mm DFT before shipment. Grade and thickness follow the corrosivity of the service, the local climate, and the target design life, because once the shell is erected the metal that carries the load cannot be re-specified without a costly rebuild.
· Material: carbon steel is the baseline; grade and thickness follow the corrosivity of drilling fluid (mud and brine) and the local climate.
· Surface prep: Plate is shot-blasted to Sa 2.5 before coating so the film bonds instead of sitting on mill scale.
· Standards: Built to API 650 and API 12F, with weld procedures and NDE matched to the code.
· Agitation: Paddle or jet mixers stop barite from settling so the fluid stays pumpable and on-spec.
· Why it matters: Once in service you cannot easily re-specify the material; the choice made here sets the maintenance curve for decades.
3. Sizing, Welding, and Inspection
A carbon steel tank earns its rating at the joint and the hydrotest, not on the sales drawing. Welds are qualified and examined over 10-100 % of their length by radiography or ultrasonics, the shell is proven under water to 1.25x the design head, and the mill certificates, NDE reports, and coating-thickness logs travel with the tank into its operating life. Inspection is what turns a fabricated shell into an asset a regulator will permit and an insurer will cover.
· Welding: Qualified welds are examined by radiography or ultrasonic testing so hidden defects do not become leaks.
· Hydrotest: The shell is hydrostatically tested to 1.25x the design head or to code, proving every course before coating and backfill.
· Mobility: Skid-mounted tanks move with the rig; coatings resist the abrasive, chemically treated mud.
· QA package: Mill certificates, NDE reports, and coating-thickness logs are compiled per tank and handed to the operator.
· Why it matters: Inspection is what turns a fabricated shell into a tank you can insure and permit.
Design parameter | Typical value or range | Why it matters |
Capacity range | 20-5,000 m3 | Single-tank throughput |
Shell plate | 6-40 mm | Hydrostatic head by elevation |
Coating DFT | 0.25-0.40 mm | Verified before shipment |
NDE coverage | 10-100 % | Seam length examined |
Vapor loss | up to 99 % | Standing-loss reduction |
Rim seal cut | ≥90 % emissions | Rim-space control |
Service life | 30-50 years | Design target |
Operating temp | 20-60 °C | Product and climate |
Code basis | API 650 | Design authority |
Limitation to check | Abrasive, treated mud | Watch this in the spec |
Wind / seismic load | 0.5-1.5 kPa | Roof and shell load |
Foundation settle | 0.1-0.3 m | Controlled subgrade |
Throughput | 50-500 m3/d | Typical draw |
Operating temp | 20-60 °C | Product and climate |
Product density | 800-950 kg/m3 | Typical range |
Design margin | 10-20 % | Allowance in steel |
Evaluation Criterion | carbon steel | Carbon steel welded | Stainless steel |
Code basis | API 650 | API 650 | API 650 |
Corrosion defense | oilfield fluid duty | Coating-dependent | Inherent |
Capacity range | 20-5,000 m3 | Up to 150,000 m3 | Up to 20,000 m3 |
Construction | welded | Welded | Welded |
Service life | 30-50 years | 30+ yr | 40+ yr |
Engineering Assurance and Project Support
Every welded oil tank delivered by Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel) is designed to API 650 with shell courses sized by the one-foot method and checked for wind, seismic and hydrostatic load cases, or to EN 14015 and the Eurocodes where the site is European. Shell plate is shot-blasted to Sa 2.5 and coated to a documented dry film thickness, longitudinal and annular plate welds are examined by radiography or ultrasonic testing to the acceptance level written into the purchase order, and every tank is hydrostatically tested and dimensionally surveyed before hand-over. Rim-seal details, coating-thickness logs, and hydrotest records travel with every drilling fluid (mud and brine) project so the design story survives audit against API 650.
A drilling fluid (mud and brine) tank is not a commodity shell; it is a structural calculation, a coating system, and an inspection record that has to hold for 30 years or more.
Frequently Asked Questions (FAQ)
What is a carbon steel drilling fluid (mud and brine) tank used for?
It stores drilling fluid (mud and brine) under controlled conditions, protecting the product from contamination and the site from release while meeting API 650 for structure and inspection.
Which standard governs a welded drilling fluid (mud and brine) tank?
The primary basis is API 650, supported by API 12F for materials, welding, and corrosion protection; local codes and permits then confirm the choice.
How is corrosion controlled on a drilling fluid (mud and brine) tank?
carbon steel is specified for the service, plate is blasted to Sa 2.5 and coated, and cathodic protection is added where soil or product demands it. The coating-thickness log is verified before shipment.
Can a drilling fluid (mud and brine) tank be customized for my site?
Yes. Shell height, roof type, nozzles, heating coils, and instrumentation are matched to throughput, climate, and code. Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel) issues drawings and an inspection package per tank.
Key Takeaways
· Match the material to oilfield fluid duty first; the coating and code follow from that decision.
· Size the shell by the one-foot method where welded or by course rating where bolted, then prove it.
· Treat welding, hydrotest, and NDE as the real rating, not paperwork.
· Keep the inspection and coating records; they are what makes the tank bankable.