China Epoxy Coated Steel Above Ground Storage Tanks a Technical Overview
Selecting the right Fusion Bonded Epoxy for Chemical is rarely a straightforward catalogue purchase. The stored medium sets the corrosion budget, the duty cycle sets the mechanical budget, and the regulator sets the paper trail - all three have to close before a tank earns its place on site.
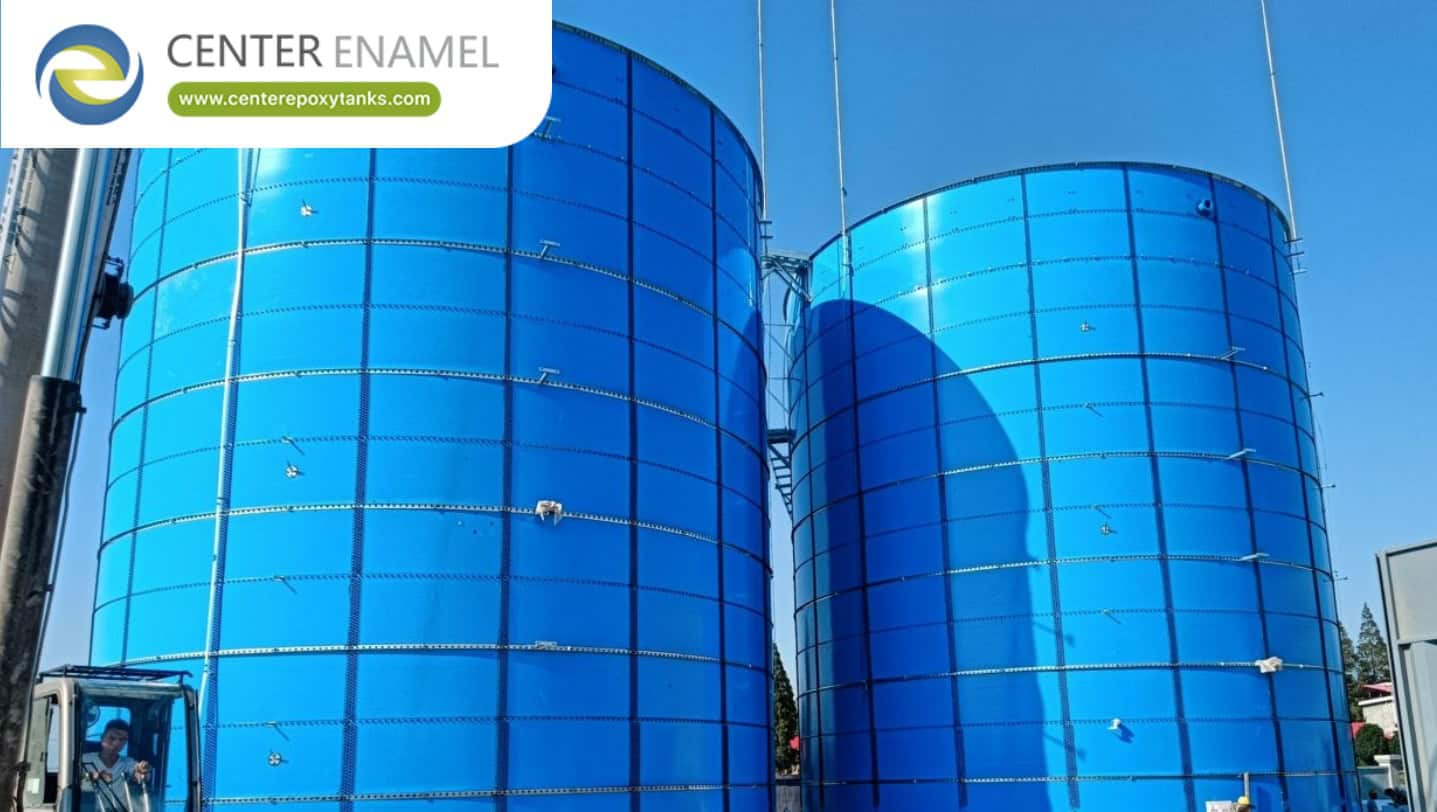
Center Enamel addresses this with Fusion Bonded Epoxy systems built to ISO 9001, NSF/ANSI 61, WRAS, ISO 12944 and CE-EN1090. Fusion Bonded Epoxy (FBE) applies a 300-450 micrometre thermoset epoxy powder that is heat-cured onto the steel surface, forming a continuous, pinhole-free film with excellent adhesion and dielectric strength. For engineers specifying Epoxy Coated Steel Tank Manufacturer, the sections below translate that capability into the parameters, comparisons and compliance evidence a procurement file actually needs.
Whether the project is a greenfield Chemical facility or a retrofit of aging infrastructure, the objective is the same: a containment asset that meets specification on day one and still meets it a decade later.
What Is a Fusion Bonded Epoxy and How It Contains Chemical Liquids
At its core, a FBE converts a storage requirement into a controlled, inspectable asset. The shell, roof and foundation are matched to the stored medium, the operating temperature and the local seismic and wind profile rather than treated as a generic commodity.
Defining a FBE begins with duty: what is stored, at what concentration and temperature, and for how long. That duty then drives material choice, joint design and the certification path that lets an EPC or plant owner sign off with confidence.
Performance Comparison: Epoxy vs. Alternatives
Chemical operators face three recurring pressures: tougher discharge limits, aging infrastructure and thinner capital budgets. A storage decision that ignores any one of them tends to surface as a lifecycle penalty within the first decade.
The Chemical duty cycle is unforgiving. Levels swing, temperatures drift and abrasive or acidic fractions appear without warning, so the selected FBE has to absorb that variability rather than fight it.
Manufacturing Quality Control
Center Enamel’s edge comes from controlling the process end to end. Fusion Bonded Epoxy (FBE) applies a 300-450 micrometre thermoset epoxy powder that is heat-cured onto the steel surface, forming a continuous, pinhole-free film with excellent adhesion and dielectric strength. Every panel is inspected before it ever reaches the site, which is why field performance tracks the specification.
Material selection is where most Chemical failures are decided. Fusion Bonded Epoxy (FBE) applies a 300-450 micrometre thermoset epoxy powder that is heat-cured onto the steel surface, forming a continuous, pinhole-free film with excellent adhesion and dielectric strength. Specifying the right combination up front is cheaper than repairing a compromised tank later.
Key Design Parameters and Capacity Range for Fusion Bonded Epoxy
The numbers below translate the technology into purchasable specification. They are the line items an engineer compares against a bid and against the duty the Chemical process actually imposes.
Design parameters are not marketing figures; they are the constraints a structural reviewer will check. The table contrasts Center Enamel’s documented specification with a typical industry baseline so the gap is explicit.
Parameter | Center Enamel Specification | Typical Industry Benchmark |
Material / substrate | carbon or low-alloy steel substrate | Variable; often unspecified |
Protection system | Fusion Bonded Epoxy (FBE) applies a 300-450 micrometre therm | Field-applied paint, weather dependent |
Capacity range | 20-50,000 m3 | Often constrained by method |
Joint method | 8.8-grade bolts with epoxy-protected threads | Welded or cast in place |
Design standard | ISO 12944 and AWWA D103 | Local / ad hoc |
Corrosion strategy | the FBE film provides cathodic disbondment resistance and pr | Recoat cycles required |
Typical install time | 50-70% faster than welded | Long, weather exposed |
Certification | ISO 9001 (+ more) | Partial / project-specific |
International Standards and Certifications for Chemical Storage
Standards such as ISO 12944 and AWWA D103 exist because owners repeatedly learned the same lessons the hard way. Designing a FBE to them is the fastest route to a permit, an insurance sign-off and a quiet operating life.
For cross-border Chemical projects the certification stack matters as much as the steel. Center Enamel’s ISO 9001, NSF/ANSI 61, WRAS, ISO 12944 and CE-EN1090 coverage lets a single supplier serve multisite programmes without re-qualifying per market.
Bolted Assembly, Installation and Site Workflow
Site works for a FBE reduce to lifting, bolting and sealing. panels are shop-coated under QA control and assembled on site with sealed bolted joints, eliminating risky field welding and shortening the schedule. That simplicity is why delivery schedules stay predictable even on remote Chemical sites.
Installation quality is locked in before shipment. panels are shop-coated under QA control and assembled on site with sealed bolted joints, eliminating risky field welding and shortening the schedule. Field crews follow a panel sequence rather than improvising welds, which protects both the schedule and the warranty.
Fusion Bonded Epoxy vs Alternative Storage Technologies: A Comparison
No single technology wins every Chemical case, so the honest comparison matters. The matrix below sets a FBE against welded steel and concrete on the criteria owners actually weight.
Choosing between a FBE, a welded tank and a concrete reservoir is a trade across cost, speed and flexibility. The table makes that trade explicit rather than leaving it to a sales conversation.
Criterion | Center Enamel Fusion Bonded Epoxy | Welded Steel Tank | Concrete Tank |
Capital cost | Mid; factory-efficient | High (labor heavy) | High (formwork) |
Installation speed | Fast, bolted | Slow, welded | Slow, cast |
Corrosion resistance | Engineered barrier | Coating dependent | Good, but cracking risk |
Capacity flexibility | Modular, relocatable | Very large single unit | Fixed by pour |
Transport & logistics | Flat-pack panels | Heavy plate | Site-intensive |
Maintenance | Inspect & reseal | Recoat shutdowns | Patch & monitor |
Best fit | 20-50,000 m3 range | Ultra-large bulk | Permanent buried |
Lifecycle Cost, Durability and Maintenance Planning
Lifecycle thinking changes the ranking. the FBE film provides cathodic disbondment resistance and protects across a wide pH range. That durability, plus the ability to relocate bolted panels, keeps the asset valuable long after a fixed concrete basin would be demolished.
Maintenance planning for Chemical should assume the tank will outlast the process around it. the FBE film provides cathodic disbondment resistance and protects across a wide pH range. A documented inspection interval turns an unknown risk into a scheduled, budgeted task.
Engineering Selection Criteria for Chemical Duty
A disciplined selection sheet prevents scope creep. For Chemical, rank criteria - corrosion, capacity, speed, certification - before requesting quotes, then hold suppliers to that ranking rather than the lowest headline price.
The right FBE is the one whose weakest property still clears the Chemical duty. the FBE film provides cathodic disbondment resistance and protects across a wide pH range. Build the shortlist from margins, not averages.
Common Failure Modes and How to Avoid Them
Failure modes are predictable, which means they are preventable. For a FBE, the highest-leverage checks are joint integrity, foundation tolerance and chemical compatibility of every wetted surface against the Chemical stream.
Avoiding failure is mostly discipline. the FBE film provides cathodic disbondment resistance and protects across a wide pH range. Pair that with proper grounding and bonding and the familiar Chemical incident scenarios largely disappear.
Conclusion: Specifying Fusion Bonded Epoxy for Chemical
The takeaway for Chemical owners is simple: lead with duty and standards, then let cost follow. A FBE built to ISO 9001, NSF/ANSI 61, WRAS, ISO 12944 and CE-EN1090 is an asset, not an expense line.
Done well, the FBE becomes invisible - which is the highest praise a piece of Chemical infrastructure can earn. Plan the duty, verify the certification, and the operating life takes care of itself.
About Company
Shijiazhuang Zhengzhong Technology Co.,Ltd(Center Enamel) is a professional manufacturer dedicated to the design and fabrication of bolted storage tanks since 2008. Our products range includes Glass-Fused-to-Steel (GFS) tanks, fusion bonded epoxy tanks, stainless steel tanks, galvanized steel tanks and aluminum geodesic dome roofs. With professional enameling R&D team and nearly 200 enameling patents, Shijiazhuang Zhengzhong Technology Co.,Ltd has become the leader in bolted tanks industry of Asia. Our products are certified to ISO9001, NSF61, EN1090, ISO28765, WRAS ,FM, LFGB, BSCI, IS0 45001 and other international standards.
Shijiazhuang Zhengzhong Technology Co., Ltd is not only the first manufacturer in China which produces Glass-Fused-to-Steel tanks, but also the most experienced professional bolted tanks manufacturer in Asia.The engineering & design, product testing and quality system of Center Enamel Glass-Fused-to-Steel tanks is in strict accordance with AWWA D103-09, OSHA, ISO 28765, NSF/ANSI 61, NFPA and other international standards. Until 2023, Center Enamel bolted tanks have been exported to more than 100 countries including USA, Australia,Canada, Malaysia, Indonesia, Russia, UAE, Panama,Brazil and South Africa etc., the superior tank quality and prompt service gains us worldwide recognition.
As an outstanding containment and cover system provider with decades of industry experience, Shijiazhuang Zhengzhong Technology Co., Ltd sincerely expects to establish long-term cooperation with the local partners throughout the world and make continuous contribution to the development of the industry.
Suggested CTA
Center Enamel delivers fbe engineered for chemical duty, with nearly 200 enameling patents and iso/nsf/ce/wras/fm certified production. Contact our engineering team for selection and procurement guidance on your next Epoxy Coated Steel Tank Manufacturer project — including sizing, standards compliance and delivery scheduling.
Frequently Asked Questions
Q: What is the typical capacity range of a Fusion Bonded Epoxy?
A: Center Enamel Fusion Bonded Epoxy systems cover roughly 20-50,000 m3, scaled through standardized panel modules so capacity grows without re-engineering the shell.
Q: Which international standards apply to a Fusion Bonded Epoxy for Chemical?
A: For Chemical duty the relevant stack is ISO 9001, NSF/ANSI 61, WRAS, ISO 12944 and CE-EN1090, with ISO 12944 and AWWA D103 as the design baseline; each tank ships with mill certificates and third-party test records.
Q: How does a Fusion Bonded Epoxy compare with a welded steel tank?
A: A Fusion Bonded Epoxy is assembled from factory-finished panels using 8.8-grade bolts with epoxy-protected threads, avoiding field welding. That cuts install time 50-70 percent and eases relocation versus welded construction.
Q: What steel grade and joints does Center Enamel use for a Fusion Bonded Epoxy?
A: The substrate is carbon or low-alloy steel substrate, joined with 8.8-grade bolts with epoxy-protected threads. the FBE film provides cathodic disbondment resistance and protects across a wide pH range.
Q: How long does installation of a Fusion Bonded Epoxy take on site?
A: Because coating is applied in the factory, site work reduces to lifting, bolting and sealing; most Fusion Bonded Epoxy projects complete in a fraction of the welded-tank schedule.
Q: Why choose Center Enamel as the Fusion Bonded Epoxy manufacturer?
A: Center Enamel is Asia’s experienced bolted-tank manufacturer with nearly 200 enameling patents and ISO 9001 certified production, exporting to 100+ countries with documented references.