Innovative Double Membrane Roofs For Biogas Digester Covers
On a modern anaerobic digester, the membrane roof does two jobs at once: it covers the digester and it stores the gas. That integration is elegant — no separate holder structure, no extra footprint — but it concentrates the engineering. The membrane must survive a corrosive headspace atmosphere, hold pressure across the operating stroke, and provide access for the inspection and mixing equipment below.
This article covers the cover as a system: the integration logic, gas tightness classes, the anti-corrosion detailing that the headspace demands, and the access provisions that keep the digester maintainable.
The Integrated Cover Concept
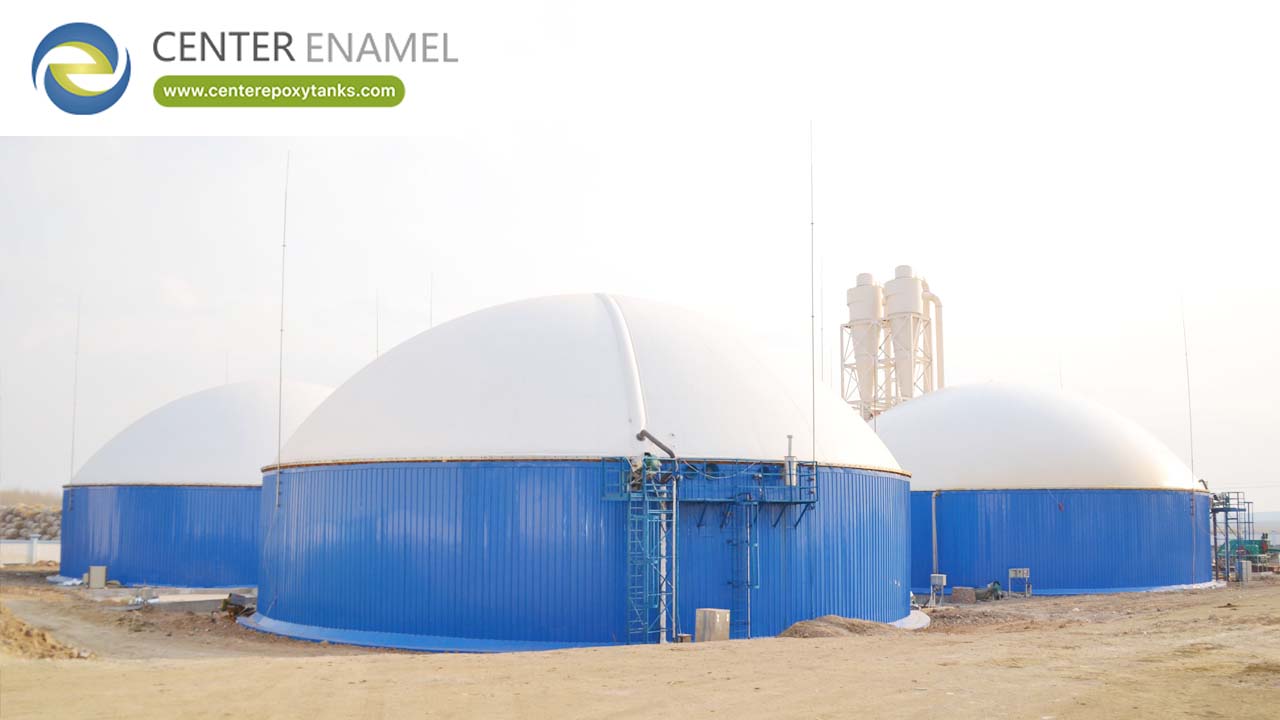
A double membrane digester roof mounts on the digester wall: the inner membrane stores gas, the outer membrane provides weather protection, and the pressurized air space between them sets the operating pressure. Gas storage capacity comes from the dome volume above the digestate surface — capacity that a conventional flat roof would waste.
The integration eliminates a structure, a foundation and a set of interfaces. It also concentrates every failure mode into one component, which is why the engineering standard for these covers is higher than for either a roof or a holder alone.
Gas Tightness Classes
Cover performance is specified by leakage rate, and the classes matter: a cover for simple gas storage tolerates more leakage than one feeding an upgrading skid or a regulated emission inventory. Leakage targets are written into the specification and verified at commissioning by pressure-decay testing.
The class decision is an economics decision as much as a technical one: tighter covers cost more to fabricate and inspect, and they pay back through reduced gas loss — which is energy, revenue and emissions all at once.
Tightness Class | Application | Verification | Cost Impact |
Standard | Simple heat storage, boiler duty | Pressure-decay at commissioning | Baseline fabrication |
Enhanced | CHP with gas quality sensitivity | Pressure-decay plus seam audit | Higher inspection intensity |
High | Upgrading skids, regulated inventory | Full seam and penetration audit | Highest fabrication standard |
Membrane System Design
The membrane system comprises the inner gas membrane, the outer weather membrane, the air pressurization system with blower and controls, and the relief set that protects both membranes. Material selection addresses the gas composition — H2S concentration and moisture — plus UV exposure for the outer membrane.
The control loop must hold pressure band across the full stroke, from empty to full, without hunting. It is the same control problem as a standalone holder, solved in a smaller volume with tighter integration.
Anti-Corrosion Detailing
The headspace above a digester is one of the most corrosive atmospheres in the process industry: H2S, moisture, CO2 and temperature cycling attack every exposed surface. Steel details in the headspace — the membrane attachment ring, access frames, mixing shaft penetrations — must be specified for the atmosphere, not for structural duty alone.
The membrane attachment is the critical interface: the ring beam, the clamp detail and the seal must hold both mechanically and gastight while the steel behind them resists the headspace chemistry. This is where covers fail, and it is where the detailing earns its fee.
Penetrations And Sealing
Every penetration through a membrane cover is a seal: gas offtake, pressure instrumentation, access hatches, mixing shaft passages and lighting. Each is detailed for gastightness, for movement (the membrane deflects under pressure change) and for inspection access.
The penetration list is the cover’s risk register. Each item is engineered, fabricated and inspected as a unit — and each is a maintenance inspection item for the life of the cover.
Penetration | Seal Requirement | Movement Accommodation | Inspection Interval |
Gas offtake | Gastight, H2S-rated | Membrane deflection range | Annual |
Pressure instrumentation | Gastight | Minimal movement | With calibration |
Access hatch | Gastight when closed | Hatch frame tolerance | Each entry |
Mixing shaft passage | Gastight, rotating seal | Shaft runout | Continuous monitoring |
Inspection Access
Digesters need internal access for mixing equipment service, heating coil inspection and cleaning. The cover must provide that access — hatches sized for equipment removal, with the membrane system designed so that access does not compromise gastightness. Confined-space procedures govern every entry.
Access design is a lifecycle decision: a hatch that is too small for the mixer is a hatch that will be enlarged by a cutting torch, with the gastightness repair that follows.
Pressure And Relief Systems
The relief set protects the membranes at both extremes: over-pressure when production exceeds offtake, under-pressure when offtake exceeds production. Relief setpoints are specified against membrane design limits, and the system is tested at commissioning and on schedule thereafter.
The blower system maintains the air space pressure that sets operating band. Its reliability is the cover’s reliability — a failed blower is a failed pressure control, and the relief system is the last line, not the operating plan.
Retrofit Covers On Existing Digesters
Membrane covers are frequently retrofitted to existing digesters: an open or flat-covered digester gains gas storage capacity and emission control without replacement. The engineering work is the interface — wall capacity for the new loads, attachment ring design and the penetration layout.
Retrofit scope includes the headspace assessment: existing steel details in the atmosphere are evaluated for corrosion condition, and the attachment design accounts for what is actually there rather than what the drawing showed.
Operation And Maintenance
Cover maintenance is the membrane regime: external condition inspection, seam and penetration checks, blower and control service, and relief function testing. The schedule is written around the digester’s operating plan, with internal membrane inspection at planned shutdowns.
The maintenance model rewards integration: one system to inspect rather than a roof plus a separate holder, and one documentation file rather than two.
Standards And Certification
Digester covers sit at the intersection of several standard families. The tank structure follows its own code — AWWA D103 and ISO 28765 for glass-fused-to-steel bolted tanks, EN 1090 for fabrication execution — while the membrane system, the pressure control and the relief set draw on gas-holder and pressure-equipment practice. Where the digester feeds a regulated emission inventory or a gas grid connection, the cover documentation must satisfy that program’s reporting requirements as well.
The practical consequence for buyers is to require the certification set at procurement, not at handover: material certificates for the membrane fabric and the steel details, welding procedure qualifications, the commissioning pressure test record and the relief setpoint certificate. A cover supplied without this set cannot be verified later, and an unverifiable cover is an unmanaged emission source.
Center Enamel Membrane Cover Engineering
Center Enamel engineers double membrane covers on operating digesters, from the gas balance and tightness class through penetration detailing and commissioning pressure testing. Our GFS digester systems are selected for their resistance to the headspace chemistry, and our membrane systems are built for the pressure control duty the digester demands.
For digester covering, the standard we hold is the one the atmosphere demands: every penetration sealed, every detail corrosion-specified, every relief setpoint verified.
Project Case Study
A Beijing biogas project required digestion capacity with integrated gas storage covering for its organic waste stream. Center Enamel supplied a glass-fused-to-steel bolted tank at 14.51 m diameter by 9.6 m height, totaling 1,587 m3, configured with a double membrane roof system providing controlled-pressure gas storage above the digestate surface.
The GFS tank system provides the vitreous enamel interior that the digester chemistry demands, while the membrane roof integrates storage capacity into the cover structure. The project was delivered complete in November 2021 with coating inspection records for the operating integrity baseline.
Project Reference | 01 China Beijing Biogas 202111 |
Location | China |
Application | Biogas Project |
Product / Technology | Glass-Fused-to-Steel (GFS) Bolted Tank |
Tank Count | 1 |
Tank Dimensions | φ14.51*9.6m(H), 1 unit |
Total Volume | 1587 m3 |
Completion | Delivered and completed 2021-11 |
Supply Scope Note | A relevance grade to this topic |
About Company
Shijiazhuang Zhengzhong Technology Co.,Ltd(Center Enamel) is a professional manufacturer dedicated to the design and fabrication of bolted storage tanks since 2008. Our products range includes Glass-Fused-to-Steel (GFS) tanks, fusion bonded epoxy tanks, stainless steel tanks, galvanized steel tanks and aluminum geodesic dome roofs. With professional enameling R&D team and nearly 200 enameling patents, Shijiazhuang Zhengzhong Technology Co.,Ltd has become the leader in bolted tanks industry of Asia. Our products are certified to ISO9001, NSF61, EN1090, ISO28765, WRAS ,FM, LFGB, BSCI, IS0 45001 and other international standards.
Shijiazhuang Zhengzhong Technology Co., Ltd is not only the first manufacturer in China which produces Glass-Fused-to-Steel tanks, but also the most experienced professional bolted tanks manufacturer in Asia.The engineering & design, product testing and quality system of Center Enamel Glass-Fused-to-Steel tanks is in strict accordance with AWWA D103-09, OSHA, ISO 28765, NSF/ANSI 61, NFPA and other international standards. Until 2023, Center Enamel bolted tanks have been exported to more than 100 countries including USA, Australia,Canada, Malaysia, Indonesia, Russia, UAE, Panama,Brazil and South Africa etc., the superior tank quality and prompt service gains us worldwide recognition.
As an outstanding containment and cover system provider with decades of industry experience, Shijiazhuang Zhengzhong Technology Co., Ltd sincerely expects to establish long-term cooperation with the local partners throughout the world and make continuous contribution to the development of the industry.
Suggested CTA
Center Enamel delivers double membrane roof engineered for biogas digester covering duty, with membrane cover engineering on operating digesters. Contact our engineering team for engineering guidance on your next double membrane digester cover project — including sizing, standards compliance and delivery scheduling.
Frequently Asked Questions
Q: What does a double membrane digester cover do?
A: It covers the digester and stores the gas in one component: the inner membrane holds gas, the outer membrane provides weather protection, and the pressurized air space between them sets operating pressure. Gas storage capacity comes from the dome volume above the digestate surface.
Q: How is membrane cover gastightness specified?
A: By leakage rate class, written into the specification and verified at commissioning through pressure-decay testing. Tighter classes are required where gas feeds an upgrading skid or counts toward a regulated emission inventory.
Q: Why is the headspace atmosphere so corrosive?
A: It contains H2S, moisture and CO2 with temperature cycling — one of the most corrosive atmospheres in the process industry. Every steel detail in the headspace, especially the membrane attachment ring, must be specified for the atmosphere rather than for structural duty alone.
Q: What penetrations must a digester cover seal?
A: Gas offtake, pressure instrumentation, access hatches, mixing shaft passages and lighting. Each is engineered for gastightness, for membrane movement and for inspection access — and each is a maintenance inspection item for the cover’s life.
Q: Can a membrane cover be retrofitted to an existing digester?
A: Yes. The engineering work is the interface: wall capacity for the new loads, attachment ring design and penetration layout. The headspace assessment is part of the scope — existing steel details are evaluated for corrosion condition before the attachment design is fixed.
Q: What maintenance does a membrane cover need?
A: External condition inspection, seam and penetration checks, blower and control service, and relief function testing on schedule, with internal membrane inspection at planned shutdowns under confined-space procedures.