High-Performance Welded Steel Tanks for Bulk Liquid Storage: Center Enamel
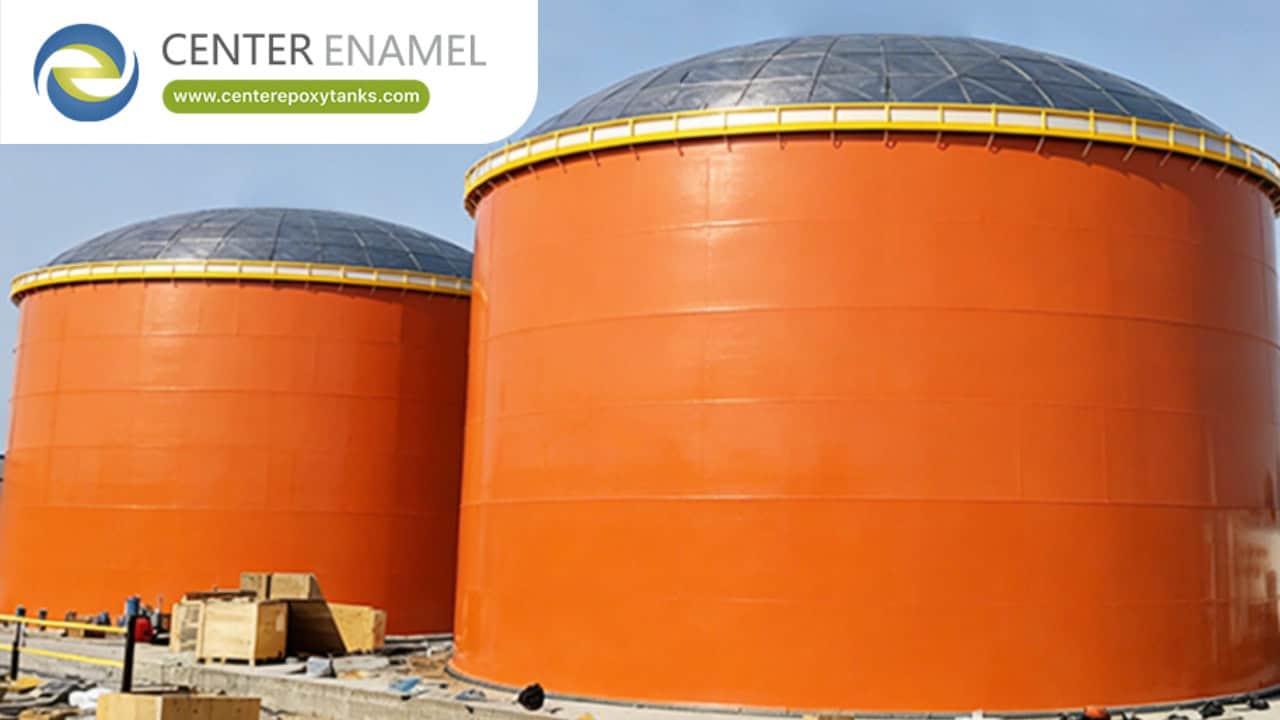
For high performance welded steel bulk liquid tanks, the right tank is defined by the stored medium, the duty cycle, and any coating or approval rule — not a single headline number. Center Enamel welds tanks to code for demanding bulk duty. A high-performance welded steel tank built with a verified coating system and correct sizing delivers a safe, low-maintenance installation.
What A Welded Steel Tank Is
A welded steel tank is fabricated from plate joined by welding, on site or in the shop, into a continuous shell. For high performance welded steel bulk liquid tanks, welding gives a monolithic structure sized from small shop-built vessels to very large field-erected tanks.
Center Enamel welds tanks to code for demanding bulk duty. Welded construction is the default for high-pressure, high-temperature, or large-diameter duties where a bolted joint is not the right choice.
Shop-Built Vs Field-Erected
Shop-built welded tanks are transported complete and suit smaller volumes and skid packages. Field-erected welded tanks are rolled and welded at the site, enabling diameters and heights that exceed road transport limits.
The split follows logistics and volume: if the tank fits a truck, shop-built is faster; if not, field welding is the path.
Design Codes And Standards
Atmospheric welded tanks commonly follow API 650 (or EN 14015 in Europe) for the shell, bottom, and roof; higher-pressure duties follow API 620 or the relevant pressure-equipment rules. The code sets plate thickness, joint efficiency, and inspection.
For potable water, verify lining and coating approvals; for flammable liquids, confirm fire separation, bunding, and venting with the authority having jurisdiction.
Welded Vs Bolted - Trade-Offs
A welded tank has no bolted seam to maintain and can suit bulk liquid storage where a seamless shell is preferred; a bolted tank erects faster, is relocatable, and gives a factory-controlled coating.
The choice weighs erection speed, relocation value, coating consistency, and the pressure/temperature envelope. Either can be correct; the duty decides.
Selection Factors
Define medium, temperature, pressure, and volume first. Choose the code, the plate specification, and the coating or lining, then confirm nozzles, roof type, and foundation with the engineer of record.
Plan welding procedure qualification, NDT, and hydrostatic test as acceptance evidence before handover.
How To Specify This Tank
1. Define the medium and duty: confirm the bulk liquid storage specifics — chemistry, temperature, solids, and any approval such as NSF-61 / WRAS for potable-adjacent duty.
2. Set the capacity from the real driver — demand, retention time, or the fire hydraulic calculation — rather than a generic rule of thumb.
3. Choose the shell and lining: a bolted, factory-coated steel tank with the lining matched to high-performance welded steel tank duty and environment.
4. Agree ancillaries and standards with the engineer of record — nozzles, roof type, level and pressure control, bunding, and the applicable codes.
5. Verify at acceptance: coating certificate, lining inspection, and a hydrostatic or gas-tightness test before handover.
Common Pitfalls To Avoid
· Specifying a size before the medium and duty are known — the lining and volume must follow the process.
· Treating the roof, membrane, or cover as a late add-on — it must be matched to the shell at design time.
· Skipping the lining inspection and pressure or hydrostatic test, which is where most lifecycle problems begin.
· Assuming one coating fits every product — verify compatibility with the actual stored medium and temperature.
Procurement, Delivery, And Commissioning
For high-performance welded steel tank in bulk liquid storage, procurement should lock the coating specification and the quality evidence — coating certificate, lining inspection, and test record — before shipment. Bolted panels arrive flat-packed; site erection is fast, and the tank can later be dismantled and re-erected if the duty or location changes.
During commissioning, confirm level and pressure instrumentation, verify the lining survived transport and erection, and document the as-built condition. A documented handover supports permitting, audit, and a sensible maintenance plan over the tank's service life.
Lifecycle, Maintenance, And Inspection
A high-performance welded steel tank is a long-life asset when the lining and structure are specified and verified for the duty. For bulk liquid storage, plan routine checks of the lining, the roof or membrane, nozzles, and level or pressure instruments, and keep a record of the as-built coating and test evidence for audit and warranty purposes.
Bolted construction makes future expansion, relocation, or re-coating straightforward compared with a welded tank. Where the medium or regulation changes, the same shell can often be re-lined rather than replaced, which protects both budget and uptime over the service life.
Technical Specifications To Confirm
Parameter | What to specify |
Medium / product | Bulk liquid storage — confirm chemistry, temperature, solids |
Capacity | From demand, retention time, or hydraulic calc |
Coating / lining | Epoxy or FBE; NSF-61 / WRAS if potable-adjacent |
Shell | Bolted steel (GFS / epoxy / stainless per duty) |
Roof | Sealed, dome, floating, or double-membrane per application |
Standards | ISO 28765, AWWA D103, NFPA 22 / EN 12845 as applicable |
Ancillaries | Nozzles, mixers, level control, bunding, access |
Center Enamel Capability For Bulk liquid storage
Center Enamel supplies bolted steel tanks — including epoxy-coated, FBE, GFS, galvanized, and stainless builds — for bulk liquid storage and adjacent duties such as fire-protection water, drinking water, municipal and industrial wastewater, and biogas. Each tank is engineered to the medium, with a factory-controlled coating, documented material spec, and lining inspection at acceptance.
· Coating systems specified per medium, including NSF-61 / WRAS where potable-adjacent.
· Bolted panels for fast erection and easy relocation or expansion.
· Relevant references: ISO 28765, AWWA D103, NFPA 22 / EN 12845 as applicable.
Frequently Asked Questions
Q: What is a welded steel tank?
A: A tank fabricated from plate joined by welding into a continuous shell, built shop-complete or field-erected.
Q: Shop-built or field-erected?
A: Shop-built if it fits transport and volume; field-erected by rolling and welding at site for larger diameters and heights.
Q: What design codes apply?
A: API 650 or EN 14015 for atmospheric tanks; API 620 or pressure-equipment rules for higher pressure; the code sets thickness, joint efficiency, and inspection.
Q: Welded vs bolted - which is better?
A: Welded has no bolted seam and suits high-pressure/high-temperature or seamless-shell needs; bolted erects faster and is relocatable with a factory coating.
Q: What acceptance evidence is needed?
A: Welding procedure qualification, NDT, and a hydrostatic test, plus coating or lining verification before handover.
Q: Can welded tanks hold flammable liquids?
A: Yes, with fire separation, bunding, and venting per the authority having jurisdiction.
High-Performance Welded Steel Tanks for Bulk Liquid Storage: Center Enamel comes down to matching the high-performance welded steel tank to the medium, the duty, and the applicable standard. Specify the lining and sizing from the real operating condition, verify the coating and hydrostatic test at acceptance, and the installation will perform.
Request A Specification
Discuss your project with a Center Enamel engineer: share medium, capacity, site, and any approval requirement, and receive a tailored tank specification and quotation.